Best Color Changing Aluminum Cup Manufacturer for Custom Drinkware Brands
2026-11-21
Custom drinkware is crowded with sameness, but a color changing aluminum cup from the right manufacturer turns an ordinary promo item into a brand moment. APEXAL approaches this niche differently: tighter color-shift control, cleaner aluminum finishing, and production runs built for brands that refuse to blend in. This guide looks at what actually separates a reliable color changing aluminum cup supplier from the rest before you commit your next launch.
Where Color Meets Aluminum Without the Usual Compromises
Colored aluminum has long meant accepting a trade-off: rich color that sits on the surface and eventually chips, or a tough finish that mutes the metal's natural character. The compromise usually comes from the layer between the pigment and the aluminum, not from the material itself.
The oxide layer is grown to a controlled depth and then sealed after color is introduced, which locks pigments inside the aluminum matrix. That means the color does not sit on top as a fragile film, and scratches or edge wear do not immediately expose raw metal.
This approach keeps saturated reds, deep blues, and muted earth tones stable under sunlight, moisture, and daily handling. It also preserves the cool, metallic feel of aluminum while removing the plastic-like gloss that often comes with protective topcoats.
Why Some Custom Cups Fade and How the Right Factory Avoids It
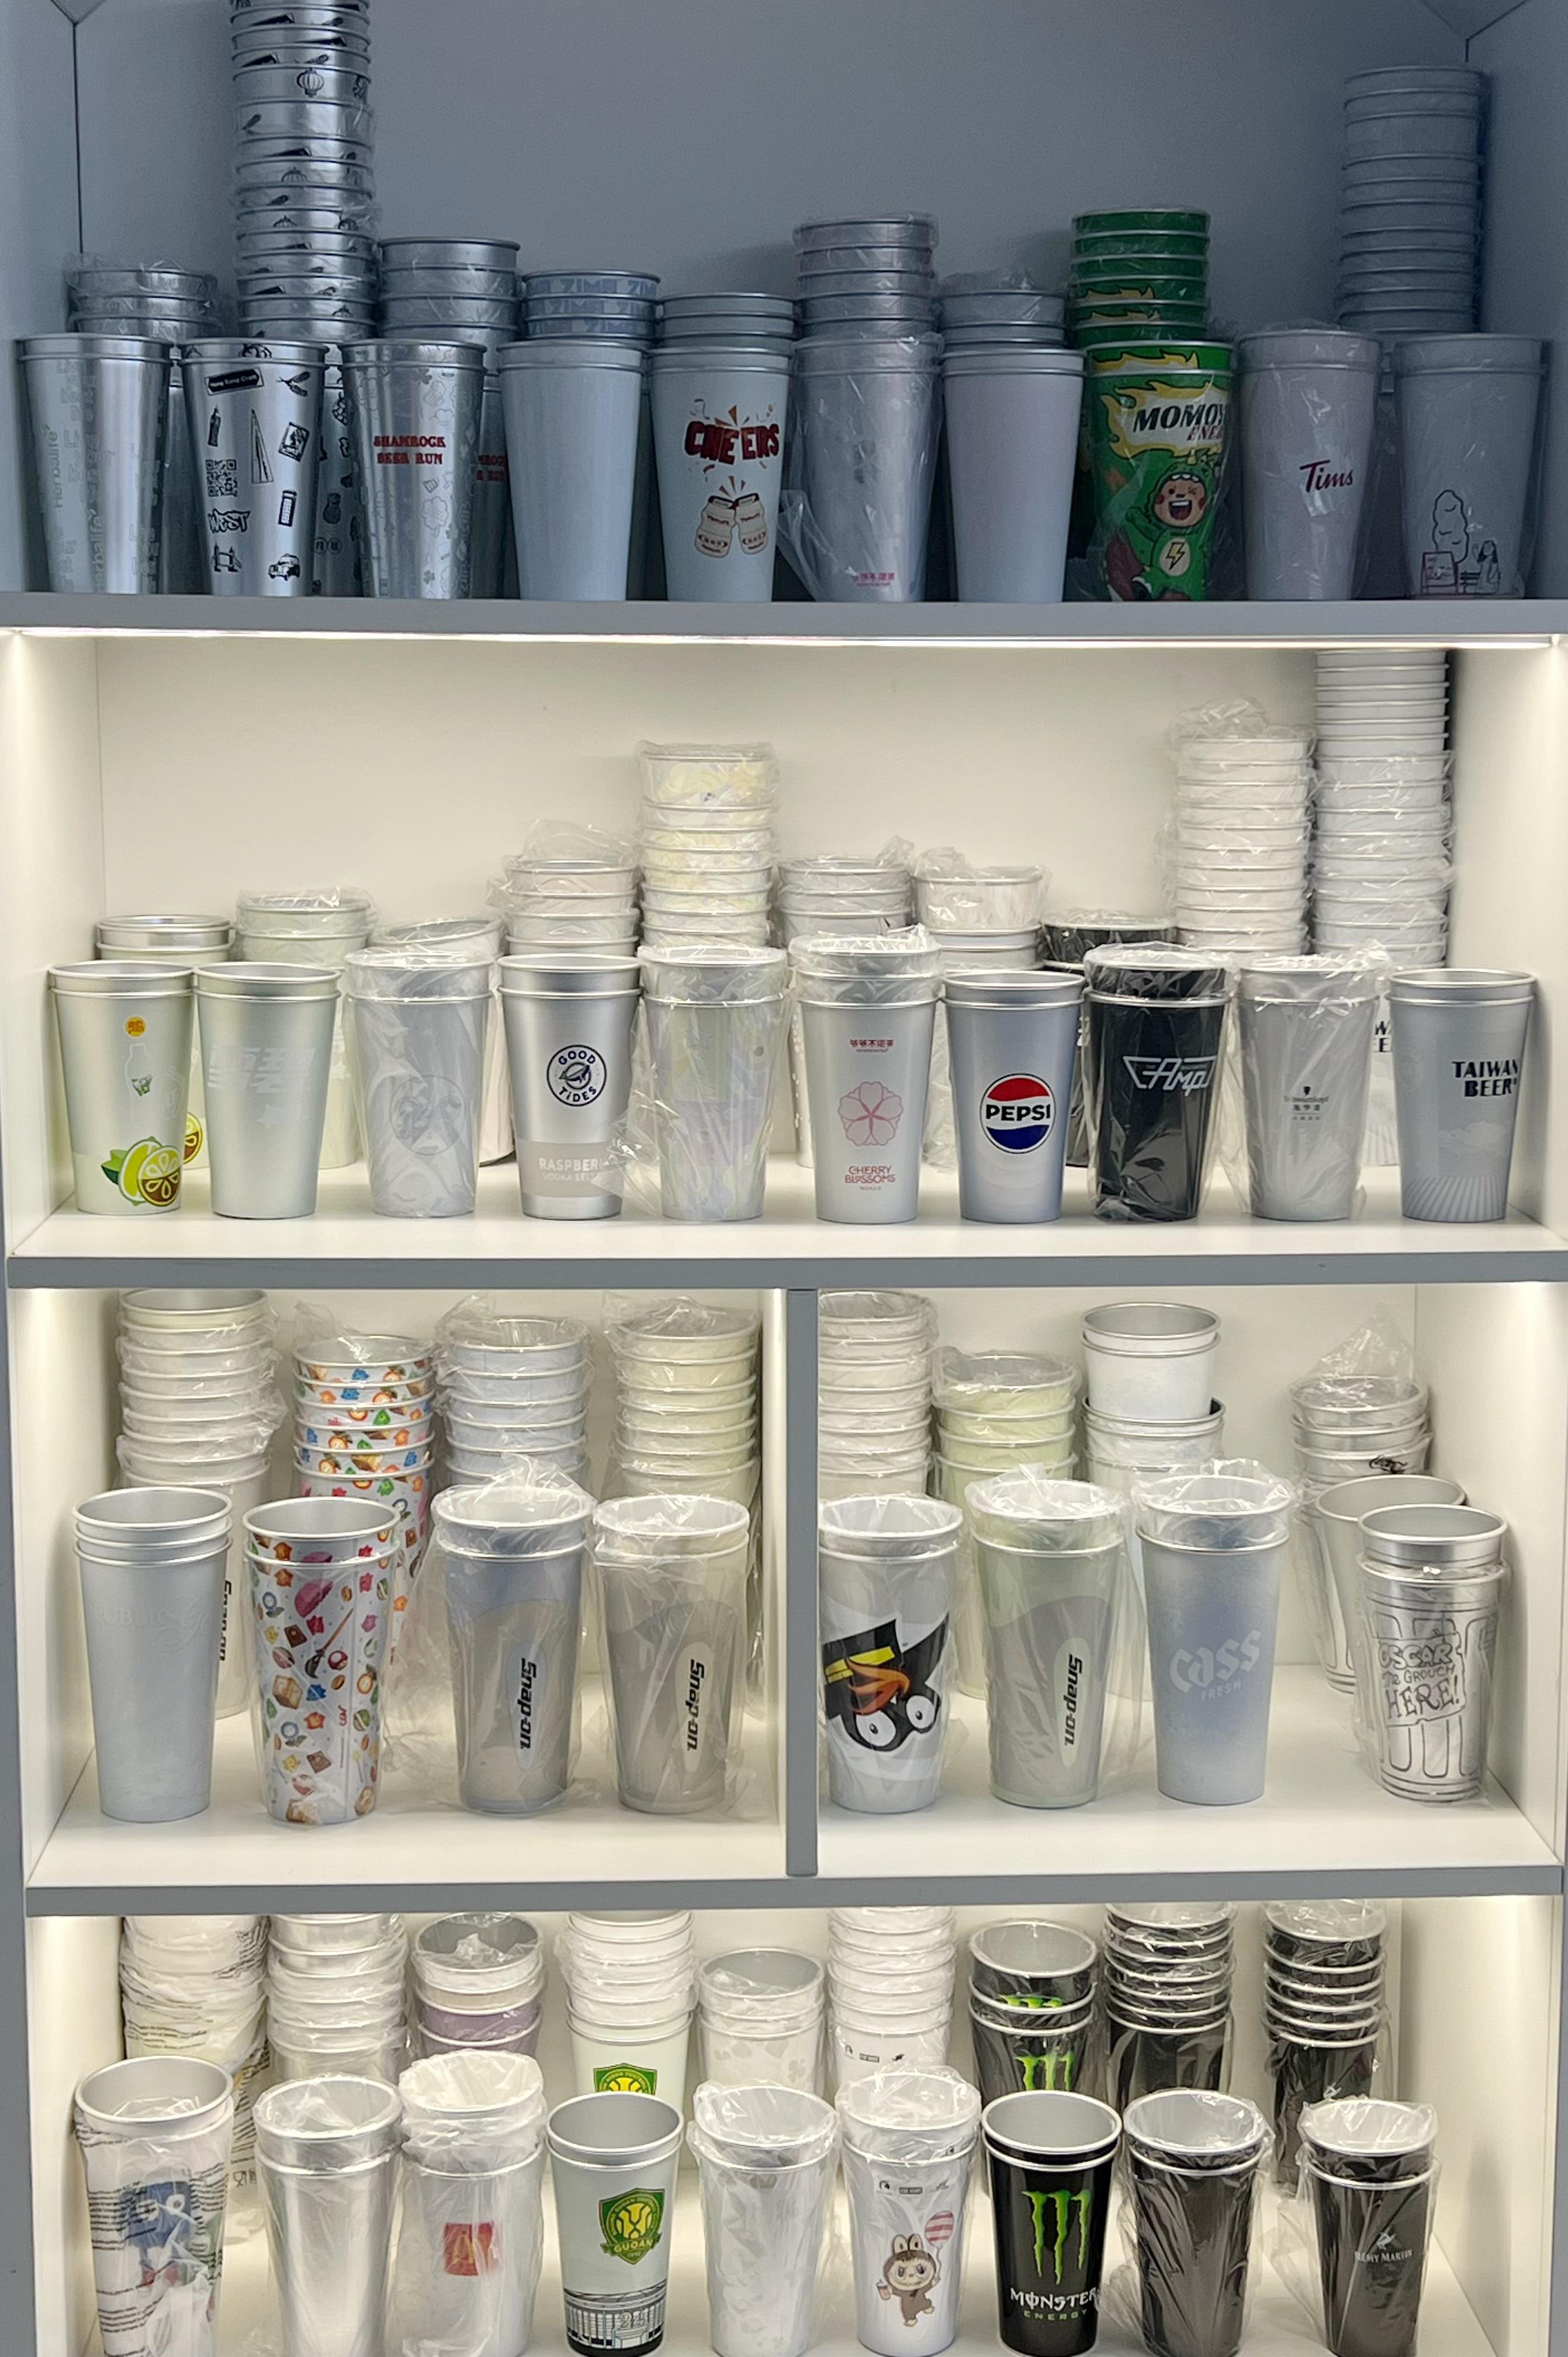
Most fading on custom drinkware isn’t a mystery. It usually traces back to shortcuts in ink selection and curing. A print that hasn’t been baked long enough or at the right temperature will look fine out of the box, but the bond between ink and cup surface stays weak. Add repeated washing, hot liquids, or sunlight, and the design starts to lift and wash out.
The substrate matters just as much as the ink. Raw stainless steel, powder-coated finishes, and plastics each need different preparation and coatings. A factory that treats every blank the same will get inconsistent results. The right partner checks surface tension, applies the proper primer or adhesion promoter, and runs sample batches through dishwashing and UV exposure tests before full production.
Long-lasting decoration also depends on process control. Small shifts in oven temperature, conveyor speed, or humidity can weaken the final cure. Shops that hold tight tolerances and log batch conditions catch these problems early. That’s the difference between a cup that still looks sharp after a year of daily use and one that starts peeling in a few weeks.
Matching Coating Effects to What Your Brand Already Stands For
Coating choice works best when it behaves like a quiet extension of the brand’s voice, not a borrowed trend. A label that already leans on raw, uncoated textures might find a soft-touch finish feels like a costume, while a crisp gloss could sharpen the existing precision of a minimalist line.
Instead of starting with a finish and forcing the identity around it, pull the finish out of what customers already touch and remember. If the brand’s story lives in warm, tactile, handmade details, a subtle grit or eggshell layer makes that story physical. If the promise is speed and clarity, a hard-wearing aqueous coating with controlled reflection can echo that same directness.
The result is a coating that doesn’t need to announce itself. It shows up as a familiar detail—consistent with the board stock, the typography, the spacing—so the finished piece feels inevitable rather than decorated. That kind of alignment tends to stick with people longer than a high-gloss novelty.
A Look Inside the Production Line for Small and Large Brand Runs
Walk the floor of a facility that handles both boutique batches and mass-market orders, and you'll notice the rhythm shifts with the run size. Small brand runs often begin at a shared prep station where operators manually load sleeves, check seam allowances, and swap thread colors between short bursts of stitching. It's a slower, more tactile pace, with each piece getting a few seconds of human attention before moving on. Large runs, by contrast, hum through automated cutting tables and multi-head embroidery units that run nearly uninterrupted, pausing only for bobbin changes or scheduled quality checks.
The real difference shows up in the transition zones. For a run of eighty units, a single line may handle everything from tag placement to final fold, and retooling takes minutes rather than hours. When the order jumps to eight thousand, the same floor splits into dedicated cells: one for panel printing, one for assembly, one for inspection under bright, angled light. Nobody is rushing between stations, but the conveyor speed and the stack heights change, and suddenly the same stitch that felt artisanal at low volume becomes a matter of repeatable tolerance.
What often gets overlooked is how the line retains a kind of muscle memory. Jigs and guides built for a large client's spec stay on the shelf, ready to be pulled down when a smaller label requests the same silhouette. And the workers who spend mornings on a 5,000-piece athletic order can, by afternoon, be hand-feeding a limited drop of two dozen jackets through a vintage chain-stitch machine. That flexibility isn't advertised on a spec sheet, but it's the quiet reason both ends of the volume spectrum leave the dock looking clean.
Private Label Cup Programs That Do Not Feel Generic
Most private label cups fail before the first sip because they start from a stock shape and a stock finish. The fastest way to avoid that is to change the hand feel: a slightly thicker rim, a lower center of gravity, a matte exterior instead of the usual gloss, or a texture that makes the cup easier to grip. These details register before the logo does, and they make the product feel specified rather than selected from a catalog.
Printing decisions also separate a generic program from an intentional one. A small, well-placed mark on the lower third of the cup can read as more confident than a full wrap printed in three colors. Even less visible choices matter, such as an ink with a soft tactility on the outside or a colored interior that changes the way the drink looks at the rim.
Consistency in small batches is the last part. When the cup wall thickness, lid fit, and sleeve texture stay predictable from one order to the next, customers stop thinking about the cup as a disposable item. Generic usually means over-decorated and under-considered; the goal is to remove visual noise while keeping the physical details deliberate.
Questions Buyers Should Ask Before Locking in a Manufacturer
Most sourcing checklists stop at price, lead time, and minimum order quantity, but those numbers mean little if the factory cannot show how they handle routine deviations. Ask to see a change notification log from the last six months: when raw material batches shifted, when tooling was adjusted, when a line supervisor changed. If the manufacturer struggles to produce that record, assume that small surprises will reach you late or not at all.
Find out who actually owns the molds, fixtures, and quality data. A factory may present a polished sample yet rely on a subcontractor for plating, assembly, or packaging. Request the full production route, including any outside processes, and ask what happens to your order when one of those partners falls behind. Also ask who is responsible for validating a new material source, and whether that requires your written approval.
Tough conversations before payment reveal more than audits. Ask about the last order that went wrong: what failed, how the factory caught it, and what compensation or corrective action the buyer received. Then ask for a recent customer reference that is in the same product category, not a generic list. If the answers are vague, walk away.
FAQ
Look at the coating process first, not just the sample photos. Ask whether the color shift is baked into the cup or applied as a thin outer layer, because that affects scratch resistance and how the cup handles repeated washing. Also confirm the factory can match your brand colors across the full cup, not only on a flat test panel.
A properly cured thermochromic coating should stay responsive for thousands of cold drink cycles if the cups are hand washed and kept out of direct sunlight for long periods. We recommend testing with iced water rather than freezers, since extreme cold can make the transition look uneven over time.
Yes. Brands can change the cup shape, rim style, lid type, base coating, and even the temperature range where the color shift happens. This is useful if you want the cup to change at a specific cold threshold that matches how your drinks are normally served.
Many manufacturers list high minimums, but it is possible to start with a few hundred units if you choose standard cup sizes and stock color combinations. Fully custom shapes and custom coating formulas usually require larger runs because the setup cost is heavier.
The aluminum body should be food-grade and paired with a protective inner coating so the drink never touches raw metal. Ask for migration test reports and confirm the outer color layer is sealed to prevent flaking near the rim where lips make contact.
The most common issue is a weak bond between the aluminum and the thermochromic layer, which causes cloudy patches or peeling after a few washes. Another issue is inconsistent color density on curved areas, so the cup looks fine on one side but faded on the other.
We work from rough sketches, existing packaging, or even a mood board. The team prepares print-ready artwork, approves a physical sample before production, and sends photos or videos of the color transition so the brand knows exactly what customers will receive.
The best results come from a soft gradient transition instead of a harsh block change, plus a smooth matte or soft-touch finish that reduces fingerprints. The cup should also have good weight and a lid that fits tightly, so the color effect feels like a detail rather than the whole product.
Conclusion
Most custom drinkware suppliers treat color-changing aluminum as a novelty, rushing a basic thermal coating onto a stock cup and calling it a day. That approach falls apart fast: uneven transitions, cloudy finishes, and fading after a few hundred washes. The better manufacturers start with the aluminum itself, using a base treatment that lets pigments bond without dulling the metal’s natural brightness. From there, coating effects are matched to what a brand already stands for—soft pastel shifts for a lifestyle label, high-contrast reveal for an energy drink, or a frosted-to-clear change for a beverage that is best served ice cold. The result is a cup that feels intentional rather than gimmicky, and it holds up under repeated use because the color layer is sealed, not just sprayed on.
Private label programs work best when the factory treats small runs and large runs with the same attention to detail. A compact order of 500 units should receive the same color accuracy checks as a 50,000-unit rollout, with the coating line adjusted for speed without sacrificing cure time. Buyers should ask how the factory tests adhesion, what happens to the color shift after exposure to heat and cold, and whether the interior coating meets food-contact standards. They should also request physical samples from the actual production line, not just pre-production prototypes. When those questions get clear answers, the custom cups stop feeling like generic merchandise and start working as a quiet extension of the brand.
Contact Us
Contact Person: Milo
Email: [email protected]
Tel/WhatsApp: +86 18621923991
Website: https://www.dgbaide.com