Bread Crumb Production Line Factory Checklist Every Buyer Should Review
2026-09-18
Most factory checklists for bread crumb production lines read like generic audit forms. They miss the practical issues that show up after installation: uneven feeding, flour dust buildup, overheating dryers, and control panels that are impossible to clean. This guide flips that approach. It highlights the checks that actually separate a durable line from a short-term bargain. If you are evaluating suppliers, these are the questions to ask before signing. And if you want to see how a manufacturer handles these details in real designs, MINGDE is a good place to start.
How the crumb size distribution shifts after three consecutive runs
After the first pass, the crumb size spread stays wide and uneven, with a visible mix of coarse fragments and fine dust. The second run starts to knock down the larger pieces, but the distribution still carries a long tail toward the coarser end. By the third consecutive run, that tail shortens noticeably and the curve pulls tighter around a smaller mean size. The change is not evenly paced: most of the reduction happens between the second and third passes, as the partially cracked crumbs from earlier runs become easier to break apart.
There is also a subtle build-up of very fine material in the third run. Some of it comes from direct fracture of mid-sized crumbs, while a portion seems to result from fines being re-compacted and then shattered again. In a few cases, overly dry or brittle crumbs produce an excess of dust that clings to the larger particles, slightly flattening the apparent size distribution near the fine end. Overall, three runs shift the curve from broad and coarse-skewed to narrower and finer-skewed, with the biggest jump in uniformity occurring after the second cycle.
Why the oven’s heat recovery setup matters more than its nameplate
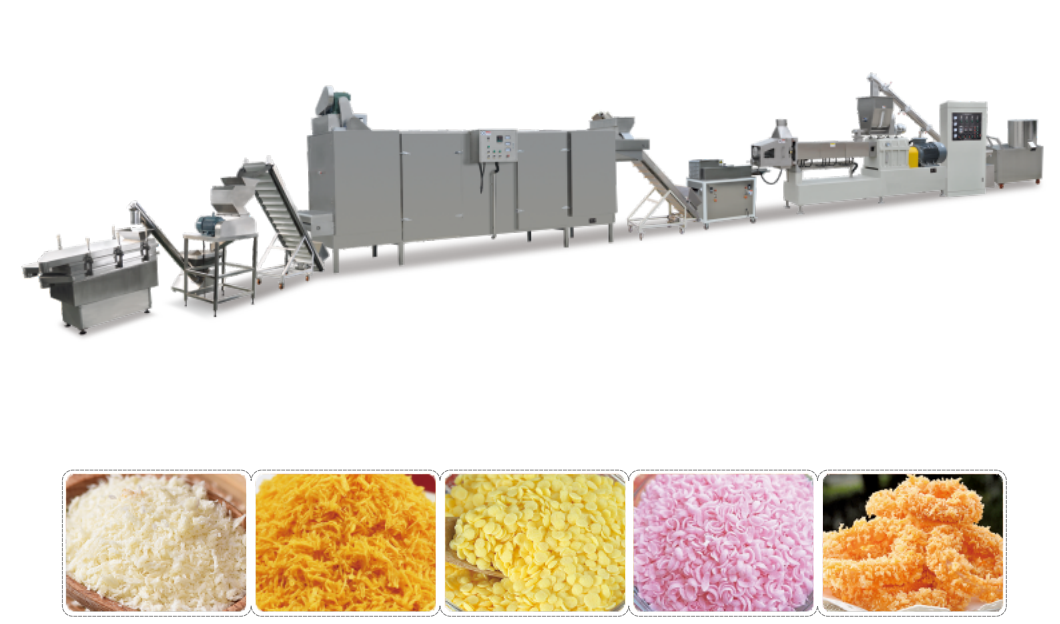
Ovens carry efficiency ratings on their badges, but those numbers rarely reflect what happens on a busy production floor. A heat recovery system can look impressive on paper, yet deliver almost nothing if the ducting forces hot exhaust through sharp bends, the exchanger surface is too small for the actual volume, or condensation isn’t drained where it forms. The nameplate figure usually comes from a steady-state test with a fixed load and clean filters. Real ovens cycle, idle, open doors, and push out moisture-laden air at changing temperatures. The setup, not the label, decides how much of that energy actually makes it back into your process.
What matters is how the recovery loop is tuned to the oven’s behaviour. A well-planned layout keeps exhaust temperature high enough to transfer useful heat without choking the burner, and it includes a bypass for when recovery would conflict with product quality. Thermal mass, insulation on return ducting, and drip legs for condensate all influence performance more than the badge rating. In many installations, a nominally lower-efficiency exchanger with short, straight duct runs and correct sizing outperforms a higher-rated unit that was simply bolted on. The setup is the system; the nameplate is only a starting point.
What the welded seams on the mixing paddles reveal about daily upkeep
Welded seams on mixing paddles rarely lie. If the beads are smooth and the surrounding metal shows no fresh grinding marks beyond normal wear, daily upkeep is probably happening the way it should—operators are scraping off product before it hardens, rinsing with the right pressure, and catching small stress cracks before they turn into breaks.
Rough, spider-webbed, or repeatedly re-welded seams tell a different story. That pattern usually means paddles are being run until failure, then patched in a hurry. It also hints at missed cleanings: hardened mix trapped next to a seam holds moisture against the weld, which speeds up pitting and makes the next patch less reliable.
None of this requires a specialist. A quick visual check at the end of a shift—looking for darkened edges, hairline cracks, or build-up along the seam—gives you a running read on whether daily upkeep is preventing problems or just covering them after the fact.
The question every buyer should ask about the cooling tunnel’s humidity
When evaluating a cooling tunnel for your production line, the humidity spec often gets buried in the datasheet under ambient conditions. But asking the right question about it can save you from sticky rejects, condensation drips, or a tunnel that never quite hits its rated throughput. The question isn't “what's the humidity range?”—it's “how does the tunnel maintain dew point control at the cold end when my product enters at 28°C and exits at 12°C, and what happens during summer startup when the factory air is already at 70% RH?”
Most buyers assume a cooling tunnel just blows cold air, but humidity inside the tunnel decides whether your product surface stays dry or weeps into the packaging. A tunnel with poor air curtain seals or undersized dehumidification will frost up on the evaporator, then dump that moisture back onto the product during defrost cycles. So ask the supplier for a psychrometric chart of the actual air path, not a single RH number—and have them walk you through a worst-case ambient scenario, like a muggy August afternoon. If they hesitate or talk only about temperature pull-down time, you've found the weak spot.
When the factory’s dust collection ductwork tells you more than the brochure
A brochure will show you a spotless floor and freshly painted equipment, but it rarely mentions the fine layer of dust caked around the duct joints or the rust blooms where condensation gathers overnight. Those details, visible only when you walk the line, reveal whether the system was designed for real production or just for the photo shoot.
Look at the ductwork elbows. Sharp ninety-degree bends with no access ports collect material and choke airflow within months. If you see heavy patchwork, mismatched clamps, or sections held together with improvised strapping, you are looking at years of reactive fixes rather than a planned maintenance schedule. The ductwork will tell you how often they actually clean it, not how often the manual says they should.
Even the sound matters. A properly balanced hood and duct run has a steady, low rush of air. Whistles, rattles, or thumping at certain sections point to leaks, collapsing walls, or undersized diameter. More than any spec sheet, these physical clues let you judge whether the facility treats dust control as a core process or as an afterthought bolted on to satisfy a checklist.
Why the emergency stop placement on the packaging line is a dealbreaker
On most packaging lines, the emergency stop is treated as a box to tick — somewhere near the main control panel, visible enough for an auditor, but rarely where an operator actually needs it. That placement becomes a serious problem the moment a film wrap jams, a carton skews, or a sealing jaw catches a stray flap. If someone has to turn away from the hazard, walk three steps, and reach around a guard to hit the button, those extra seconds are the difference between a minor stoppage and a crushed hand.
The real dealbreaker isn't just the delay — it's the mixed message it sends. When the emergency stop sits far from the infeed, discharge, or any point where operators regularly intervene, people stop treating it as a real safety device. They improvise: reaching into moving parts to clear a jam, using a foot to nudge a box, or bypassing interlocks because the official stop feels too far away. Over time, that breeds exactly the kind of shortcuts that turn a near-miss into a recordable injury.
Worse, the placement often ignores how the line actually runs on a daily basis. Packaging crews work in tight spaces, often between conveyors and palletizers, with only seconds to react. A stop button mounted on a distant electrical cabinet or tucked behind a light curtain post is effectively useless in a real emergency. If the line's safety assessment doesn't include operator reach distance, body positioning, and common jam points, then the emergency stop placement isn't just poor design — it's an active hazard that should stop the project before it starts.
FAQ
Start with the product contact surfaces. Anything touching the crumb should be 304 or 316 stainless steel, with no mild steel, flaking paint, or rusty fasteners nearby. Then follow the flow from mixing and baking to crushing and sieving to see where fines build up or where cross-contamination could sneak in.
Ask to see temperature logs from at least three full production runs, not just a demo batch. Look for hot spots by checking moisture readings at the start, middle, and end of the dryer. If the spread is more than about 1.5% moisture, you will likely get uneven browning and inconsistent crumb texture.
Find out how often the screens are inspected and replaced, and whether the crusher has quick-release guards for cleaning. Ask what happens when a screen tears during a run. If the answer is just 'we have a metal detector downstream,' that is not enough; you need to know how fast the line stops and whether the bad product is isolated automatically.
Request the HACCP plan, cleaning validation records, pest control logs, and any third-party audit certificates like BRC or SQF. Do not just accept the certificate on the wall. Ask for the two most recent corrective action reports so you can see what actually went wrong and how the factory responded.
Run a timed trial where the line produces for at least four hours without stopping. Watch the start-up and changeover, not just the steady-state speed. Calculate actual output from packed, finished product, not from raw material input. Many factories quote capacity based on ideal conditions that rarely happen.
Ask whether the line is wet-cleaned or dry-cleaned and how long a full teardown takes. Look for dead zones like hollow rollers, unsealed control panels, or overhead ledges above open product. If the factory runs gluten-free or allergen-free crumbs, ask for a validated cleaning procedure and swab results, not just a signed checklist.
Check the sensitivity settings for ferrous, non-ferrous, and stainless steel test pieces, and ask to see the actual challenge tests done at shift change. Make sure the reject mechanism can handle the crumb flow rate without backing up. Also look for magnets placed before the final packer and ask how often they are cleaned and logged.
Get a list of recommended critical spares like screens, belts, bearings, heating elements, and sensors. Confirm the supplier can ship those parts within 48 hours and ask for the names of two existing customers who have run the same line for at least a year. The agreement should also cover training time, commissioning support, and a clear performance test protocol with pass/fail criteria.
Conclusion
After three consecutive runs, the crumb size distribution shifts in ways that expose sieve wear and airflow instability far better than a static spec. A line worth buying holds its cut points steady; if fines accumulate or oversized pieces begin sneaking through, you're looking at damaged screens or uneven feed rates. The oven's heat recovery setup matters more than its nameplate rating because actual exhaust-to-makeup-air balance dictates both energy draw and browning consistency. Scrutinize the welded seams on mixing paddles too—rough, cracked, or pitted welds are not just surface flaws. They signal skipped daily inspections, and a loose weld can shed metal into the crumb stream.
The cooling tunnel's humidity deserves a direct question, not a brochure glance. If the dew point isn't tightly controlled, crumbs will clump in bags or sweat during storage, ruining shelf life no matter how crisp they came out of the oven. Also inspect the dust collection ductwork with your own eyes. Undersized, tangled, or flour-caked ducts reveal a factory that treats housekeeping as an afterthought, which raises both contamination and explosion risks. Finally, the emergency stop placement on the packaging line is non-negotiable. If operators can't reach it instantly from both the infeed and discharge sides without crossing moving parts, walk away. That one layout flaw can turn a routine jam into a serious injury, and no amount of polished equipment makes up for it.
Contact Us
Contact Person: LILY SUN
Email: [email protected]
Tel/WhatsApp: 0086-13969103791
Website: https://www.snackfoodmachinery.com/