Busbar Insulator Solutions for Reliable Electrical Power Distribution
2026-09-17
Every reliable power distribution system hides a network of small components that often go unnoticed—until one of them fails. Busbar insulators fall squarely into that category. They don't just hold conductors apart; they guard against short circuits, thermal stress, and premature equipment failure. But not all insulators are created equal, and choosing the wrong one can quietly erode system reliability. At MOLDVOLT, we engineer busbar insulator solutions to withstand real-world electrical and mechanical demands, so your distribution network stays stable when it matters most. Here’s what goes into that difference.
Material Shortlist: Epoxy, Porcelain, and the Hybrids in Between
Epoxy and porcelain rarely share a spec sheet, but they keep ending up on the same shortlist for good reason. Epoxy brings a seamless, high-gloss finish that can be poured over existing surfaces, hides subfloor imperfections, and shrugs off moisture. It also scratches under heavy furniture and can amber over time in direct sun. Porcelain, by contrast, is fired until it becomes nearly glass-hard, resists stains and heat, and handles freeze-thaw cycles without complaint. Its downsides are equally clear: cold underfoot, brittle edges, and grout lines that demand attention.
The hybrids in between try to grab the strengths of both while discarding the worst habits. Some are compact mineral slabs with resin binders that can be cut into larger-format tiles or full-height panels, giving you fewer joints than porcelain but more rigidity than poured epoxy. Others use a porcelain body topped with an epoxy-based coating or a mineral-filled core wrapped in a printed decorative layer. None of them are magic. A composite slab may still chip at the corner if you drop a cast-iron pan, and a resin-rich surface won't match the heat tolerance of true porcelain. The choice usually comes down to which failure you'd rather live with, and which maintenance rhythm fits your daily routine.
Beyond the Datasheet: Creepage and Clearance in Practice
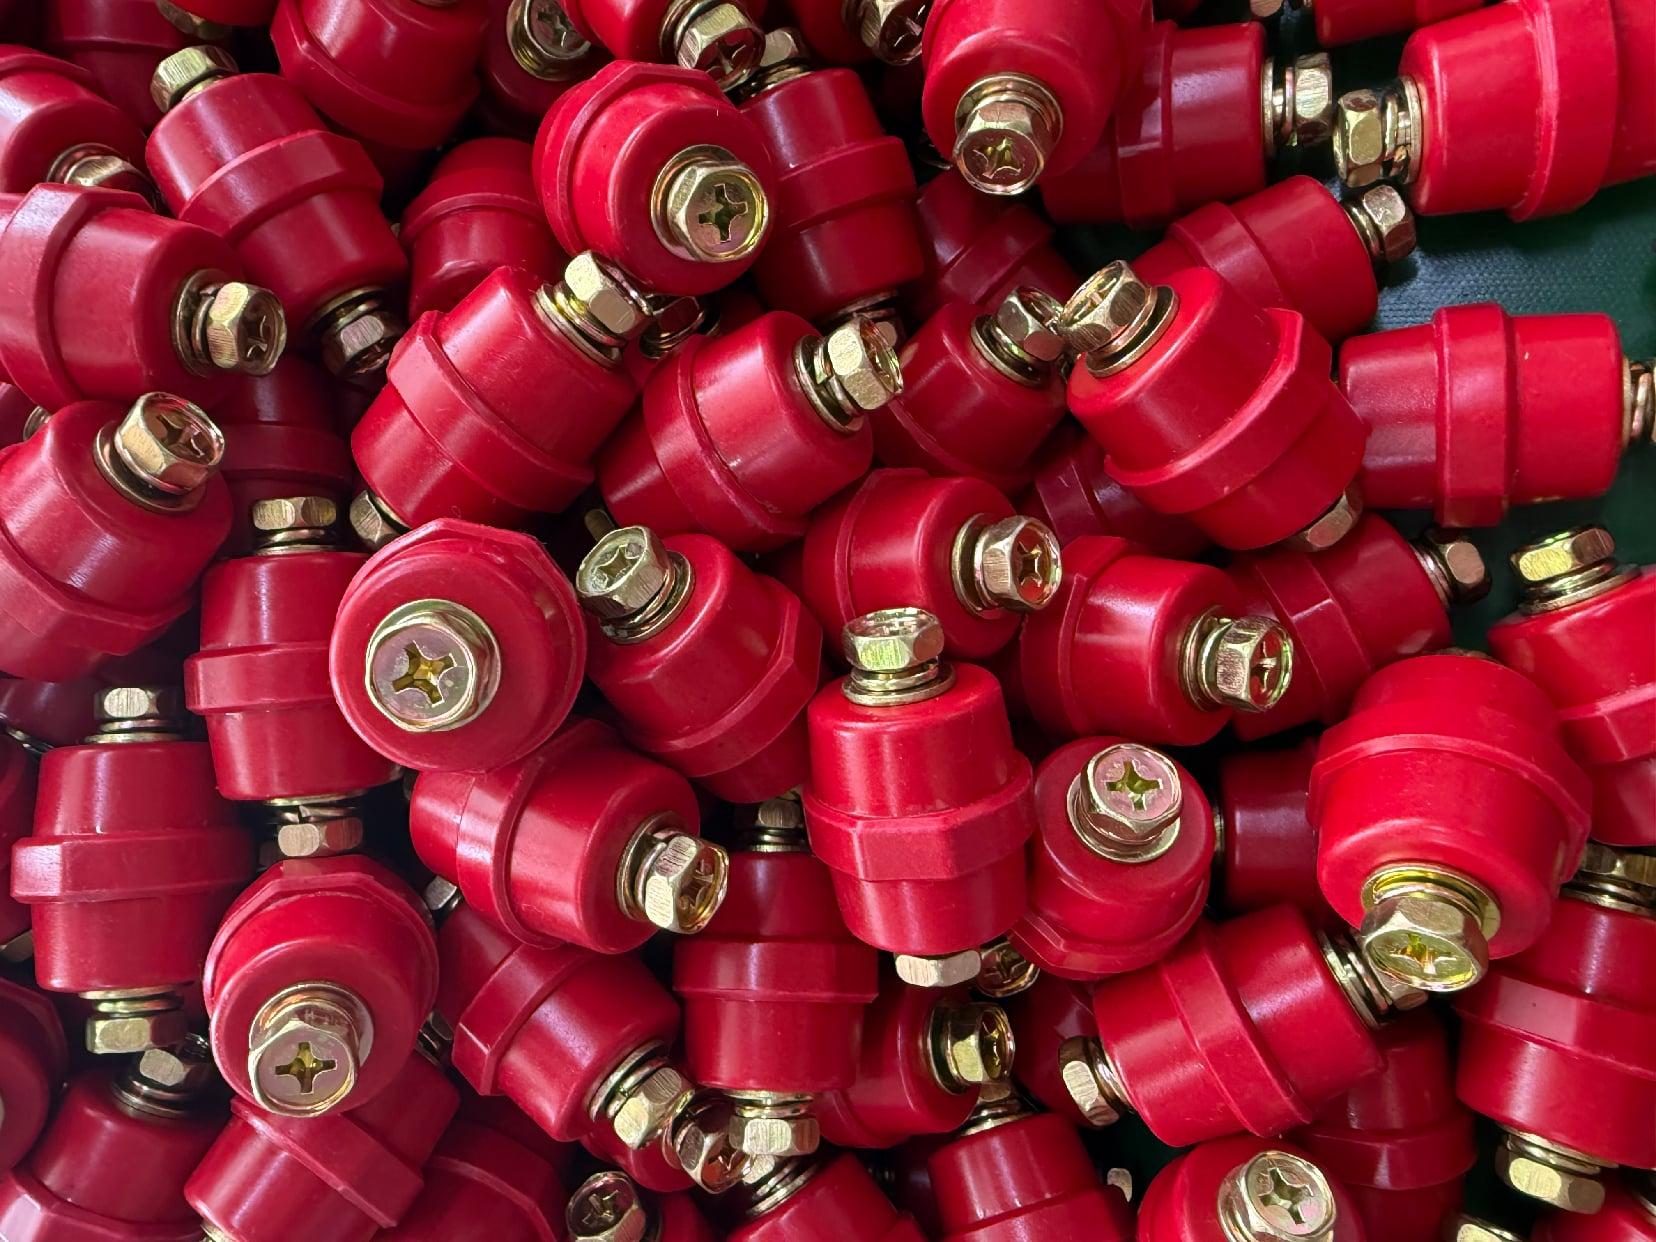
Real boards rarely behave like the idealized drawings in a component datasheet. On paper, a 3.2 mm creepage distance may satisfy a 250 V working voltage under pollution degree 2, but the same spacing can fail prematurely once dust, solder flux residue, or condensation settles on the surface. In high-voltage power supplies and motor drives, field failures often trace back to designers who used the minimum clearance from a datasheet and stopped there. A more practical approach starts by examining the actual operating environment: uncoated boards in humid industrial enclosures, silicone potting that shrinks over time, or conformal coating that cracks around tall components all shorten the effective creepage path in ways no datasheet accounts for.
Material choices and PCB surface conditions also shift the numbers significantly. Solder mask is not an insulator, and assuming it adds to creepage distance is a common mistake. A bare FR-4 surface has a comparative tracking index around 175-225 V, but contaminated or carbonized spots can drop that value locally, encouraging arc tracking. Many engineers are surprised to learn that the same 400 V circuit may require nearly double the creepage distance when moving from pollution degree 1 to pollution degree 3 as defined in IEC 60664-1. Altitude plays a subtle but critical role too: above 2000 m, the reduced air density lowers the dielectric strength, so clearance distances need a correction factor. For a product deployed at 3000 m, the datasheet-derived clearance often falls short by 10-15%, which can lead to intermittent breakdown during voltage transients.
Going beyond the datasheet means validating the design under conditions closer to real life. Instead of relying solely on calculated spacing, some teams apply partial discharge testing or 1.2/50 µs impulse voltage tests to catch weak points like sharp pad edges or closely spaced vias. Adding milled slots in the PCB between high-voltage nodes is a cheap and effective way to extend creepage without consuming board area. Another overlooked trick is to stagger component placement or rotate a package so that its exposed high-voltage terminal faces away from a nearby ground plane. In practice, a 25-30% margin above the minimum datasheet values is not wasteful; it is the difference between a board that passes a bench test and one that survives five years of thermal cycling, pollution, and voltage spikes.
Space-Saving Mounts That Don't Compromise Insulation
Mounting hardware often forces a trade-off between staying compact and keeping thermal breaks intact. Standard brackets and rails can create direct paths for heat to escape or cold to seep in, undermining the very insulation they're meant to support. The better approach uses standoff designs that grip the panel edges without piercing the insulating layer, or thermally broken clips that separate the outer flange from the inner anchor point. This way, the mount stays slim and unobtrusive while the insulation continues to perform as if nothing was attached.
For walls and ceilings where every inch counts, slim-profile channels made from low-conductivity composites or stainless steel alloys do the job without adding bulk. They're engineered to hold panels firmly against the substrate while leaving the insulation continuous behind them. The key is in the fastener placement: screws and bolts are positioned so they never cross the insulation plane, or they're fitted with thermal caps and washers that minimize heat transfer. That means you get a secure, space-saving installation without sacrificing the R-value you've worked hard to achieve.
In practice, these mounts let you keep interior dimensions generous while still meeting strict energy codes. You don't need to build out extra framing just to accommodate bulky hardware, and you don't have to choose between a tight envelope and a clean sightline. Whether you're installing insulated metal panels, exterior cladding, or interior acoustic boards, the right low-profile mount preserves both the thermal barrier and the usable square footage. It's a quiet detail, but one that makes a real difference in both comfort and long-term energy costs.
Heat, Load, and Time: The Triple Threat to Insulator Integrity
Thermal stress rarely arrives alone. On a polymer insulator, heat does more than soften the housing; it widens the gap between fiberglass core and rubber sheath, letting moisture wick inward. Repeated thermal cycling works the interface like a fatigued hinge, and the oxidation that follows can turn a once-flexible weathershed brittle long before any visible crack appears.
Mechanical load adds a second front. Conductors tug, wind gusts twist, and ice loads pull insulators into shapes they were never meant to hold for long. Under that sustained tension, microvoids in the resin open up, and the core begins to creep. If the ambient temperature is already high, the creep rate climbs sharply, because heat lowers the matrix modulus and lets the load do its damage faster.
Time is the quiet multiplier. Years of ultraviolet exposure, partial discharge, and moisture ingress leave a cumulative record that no single inspection catches. A unit that survives one hot summer or one ice storm may still fail after a decade of small insults stacking up. The real threat is not any one factor in isolation; it is the way heat lowers the threshold, load provides the stress, and time makes the damage permanent.
Failure Patterns Worth Knowing from Real Electrical Rooms
Real electrical rooms rarely fail from a single dramatic cause. Instead, they accumulate small compromises: a slightly loose lug that heats and cools until the contact resistance climbs, a vent blocked by a forgotten box, or a breaker that never gets exercised because the shutdown is too inconvenient. These quiet degradations often go unnoticed until a load step or a hot day pushes the equipment past its weakened limit.
One recurring pattern is thermal runaway at connection points. When a bolted joint loosens under vibration or thermal cycling, the resistance creeps upward. Current continues to flow, so the joint becomes its own small heater. That extra heat accelerates oxidation and further loosening, and within months a connection that passed a torquing check is now glowing under an infrared camera. The failure looks sudden in the incident report, but the trend was visible in maintenance logs for a long time.
Another pattern is the gradual loss of cooling margin. Electrical rooms are often treated as storage space, with file boxes blocking intake grilles or a new partition wall cutting off airflow. The equipment tolerates this for years because it rarely runs near its rated capacity. Then a process expansion adds load, summer temperatures climb, and breakers start tripping on thermal overload. The root cause is not the new load alone, but the accumulated loss of heat rejection that made the room unable to handle what it was originally designed for.
Predictive Checks That Keep Busbar Insulators in Service Longer
Busbar insulators rarely fail without warning. The trick is learning to read the subtle signals they send long before a flashover or crack appears. Instead of waiting for a scheduled outage or a visible breakdown, field teams now use handheld thermal cameras and ultrasonic detectors during routine walk-throughs. A slight temperature rise on one insulator compared to its neighbors often points to internal moisture or contamination that hasn't yet caused surface tracking. Catching this early means a simple cleaning or re-coating, not a full replacement.
Partial discharge monitoring adds another layer. Portable sensors placed against the insulator shed can pick up the tiny electrical bursts that occur when insulation begins to degrade under stress. These discharges are inaudible to the human ear but show up clearly on a spectrum analyzer. Over time, crews build a baseline for each busbar section. Any deviation from that baseline, even a few picocoulombs, triggers a closer inspection. This shifts the maintenance mindset from "fix it when it breaks" to "watch it before it breaks."
The real payoff comes from trend data. One utility logged thermal and acoustic readings on the same set of insulators for three years. They noticed that insulators exposed to coastal salt spray degraded twice as fast as those inland, even if all passed the standard dielectric test. By adjusting cleaning intervals and applying hydrophobic coatings only where needed, they cut unplanned outages by 40% and extended average insulator life by nearly a decade. Predictive checks turn a passive component into an active part of system reliability planning.
FAQ
The critical factors are creepage distance and the resin system. A well-designed insulator holds its dielectric strength even when conductive dust and humidity settle on the surface, so leakage currents never form a track.
Cycloaliphatic epoxy and glass-reinforced polyester lead the field. Both resist surface tracking and UV exposure, and they do not absorb moisture the way older ceramic or phenolic parts sometimes do.
Horizontal runs collect dust more easily, so you need extra creepage or periodic cleaning. Vertical installations shed contamination naturally, allowing a slightly smaller profile for the same voltage rating.
Yes, if the core is properly bonded to the metal inserts. Look for designs with a high cantilever strength rating and a flexible resin that can absorb the sudden mechanical shock without micro-cracking.
Most are fit-and-forget, but an annual visual inspection in dusty plants is worth it. Wipe down any accumulated grime with a dry cloth and check for hairline cracks near the metal flanges.
Those ribs break up the continuous conductive path that moisture and dirt can create. They increase surface distance without adding length, which is critical in compact switchgear.
Start with the system voltage and the pollution degree of the installation site. In heavy contamination, you multiply the base creepage by a safety factor, then verify against local standards for the specific insulation class.
Conclusion
Busbar insulator selection rarely comes down to a single spec sheet. Epoxy dominates many modern switchgear designs because it molds into complex shapes and holds threaded inserts well, but porcelain still earns its place in high-temperature or heavily polluted environments where surface hardness resists tracking. Hybrid materials attempt to split the difference, layering epoxy around a ceramic core or using filled resins to improve arc resistance. Beyond the datasheet, creepage and clearance need to be checked in the actual enclosure orientation, not on a bare bench. Dust accumulation, condensation patterns, and busbar proximity can halve the effective insulation distance. Space-saving mounts work only when the shortened path doesn't force a smaller creepage distance; low-profile insulators with ribbed skirts or offset mounting feet can fit tight compartments while keeping the protected path intact.
Long-term reliability faces heat, mechanical load, and time as a combined stressor. Thermal cycling loosens bolted connections, encourages micro-cracking at resin-to-metal interfaces, and accelerates pollution buildup. In real electrical rooms, common failure patterns include carbon tracking that starts at the busbar clamp, partial discharge erosion where the conductor meets the insulator body, and hairline cracks radiating from mounting holes after fault-current forces. These are rarely random; they cluster around points of repeated thermal expansion or high electrical stress. Predictive checks tailored to these failure modes outperform generic visual inspections. Infrared scans under full load reveal resistive heating at a degrading joint before it becomes a fault, while surface resistance measurements and torque checks catch early signs of contamination or loosening. Scheduling these checks after seasonal load peaks or known switching events keeps busbar insulators in service longer without unnecessary downtime.
Contact Us
Contact Person: Hellen
Email: [email protected]
Tel/WhatsApp: 86-13634205622
Website: https://www.voltcabinet.com