Industrial High Tenacity Recycled Polyester Filament Yarn: A Complete Guide to Durable, Sustainable Performance
2026-10-20
Strength and sustainability rarely sit together in industrial textiles. High tenacity recycled polyester filament yarn is changing that. This guide breaks down how it delivers the toughness heavy-duty applications demand—without the environmental cost of virgin polymer. From production methods to real-world performance, we explore what sets this material apart. And with suppliers such as Changshu Polyester refining the process, recycled no longer means a compromise. Ready to see what durable, responsible performance actually looks like?
Why High Tenacity Changes the Game for Recycled Polyester
For years, recycled polyester carried a quiet assumption: it was the eco-conscious choice, but you’d trade away some toughness. High tenacity flips that equation. By carefully controlling melt spinning and drawing, the molecular chains align more tightly, giving fibers a tensile strength that rivals—and sometimes surpasses—virgin polyester. This isn’t just a marginal bump; it opens doors to demanding applications where standard recycled polyester would tear, fray, or fail.
The real shift shows up in product lifetimes. High tenacity recycled polyester resists abrasion, tension, and repeated stress far better than its conventional counterpart. That means outdoor gear, luggage, automotive textiles, and industrial fabrics can finally lean on recycled content without compromising reliability. Every extra season of use delays landfill and offsets the need for new raw material—so the environmental benefit compounds rather than stalls.
Manufacturers no longer have to choose between performance and sustainability. High tenacity gives recycled polyester a seat at the table with premium synthetics, which changes how designers specify materials. What was once a niche alternative is now a drop-in solution for high-stress end uses, and that’s exactly the kind of momentum that turns recycled fiber from a token gesture into a genuine industry standard.
From Waste Bottles to Load-Ready Filament
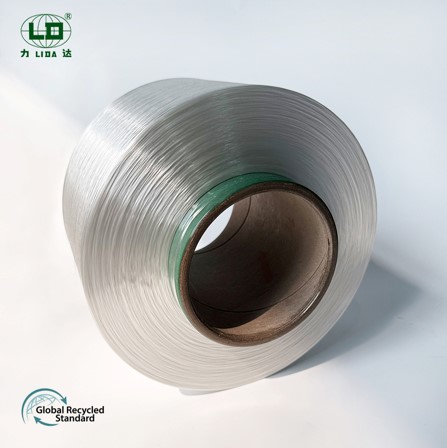
Turning old soda bottles into something your printer can actually use starts with cleaning and sorting. Clear PET containers are stripped of labels and caps, then run through a grinder that reduces them to flakes roughly the size of cornflakes. Those flakes get washed again to remove glue and residue, because any leftover sugar or soap will show up later as bubbles or weak spots in the printed part.
After drying, the clean flakes move into an extruder that melts them at a controlled temperature and pushes the melt through a fine nozzle. The trick here is keeping the diameter steady while the plastic cools and is wound onto a spool. A slight speed mismatch or a cold draft is enough to create thin sections that snap under tension, so the line runs through a laser gauge and a tension sensor before the filament is declared ready.
The finished spool loads like any other 1.75 mm material, but it brings a different personality to the build plate. Parts printed from recycled PET tend to feel slightly softer and more flexible than virgin PETG, and they handle sanding and painting well. If you have ever wanted to close the loop between what you toss in the bin and what you feed into a printer, this is a practical way to start.
The Numbers Behind Tenacity, Elongation, and Abrasion Resistance
Tenacity is usually reported in cN/dtex, and that single unit tells you how many centinewtons a single decitex filament can take before it snaps. A commodity polyester staple sits around 4.5–6.0 cN/dtex, while high-tenacity nylon 66 climbs past 8.0. But those are just dry figures; wet losses matter too—some natural fibers drop 15–20% when soaked.
Elongation at break is the percentage a material stretches before failure. Cotton rarely exceeds 8%, so it snaps with little warning. Polyester and nylon typically fall between 15% and 30%, giving them a yielding, forgiving character. Elastane is the extreme case: 400–700% elongation means it can stretch to several times its resting length and still recover, which is why it is blended at 2–5% into denim or activewear.
Abrasion resistance is usually expressed in cycles to failure on a Martindale or Taber rig. Heavy upholstery fabrics are often specified for 30,000 Martindale cycles; lightweight brushed fleece may fail below 5,000. Coated nylon packcloth can exceed 50,000 Taber cycles with a CS-10 wheel, but that same number is meaningless without the load and wheel specified.
Industrial Settings Where This Yarn Earns Its Keep
Inside paper mills, the dryer section is brutal on textiles. Felts and carrier fabrics stitched with this yarn hold their seam integrity through relentless heat, moisture, and tension. Weeks of continuous rotation leave ordinary threads stretched and frayed, but this one keeps the sheet moving without snaps or misalignment.
Automotive assembly lines put the yarn to work in cable jackets and reinforced conveyor belts. It shrugs off constant flexing, oil splash, and metal shavings that would chew through lesser fibers. Maintenance crews notice fewer unplanned stops because the yarn doesn't crack or delaminate under robotic arm repetition.
Chemical processing plants rely on filter cloth woven from the same yarn. Exposed to aggressive acids, alkalis, and high-pressure backwashing, the fabric stays dimensionally stable. That stability means longer intervals between changeouts, less downtime, and fewer leaks at the plate-and-frame seals.
How It Compares to Virgin Polyester and Nylon
Unlike virgin polyester, which starts from petroleum and carries a heavier carbon footprint, this material often begins with discarded textiles or fishing nets. The difference shows up in both energy use and water consumption: producing it can cut water usage by up to 90% compared to virgin polyester, while diverting nylon waste from landfills. But that doesn't mean it's automatically softer or weaker. In abrasion tests, it holds up nearly as well as virgin nylon, though it may have a slightly lower melting point than virgin polyester, which affects ironing and high-heat drying.
When you put it side by side with virgin nylon, the biggest surprise is how little you lose in tensile strength. Virgin nylon still edges ahead in extreme stretch recovery, but this material matches it in everyday wear—backpacks, swimwear, jackets—without the same chemical smell that virgin nylon sometimes has out of the package. Against virgin polyester, the hand feel is less slick, closer to a matte cotton blend, which some people prefer for activewear because it doesn't cling as much when damp.
Cost is another factor, though it's not as simple as "recycled is always more expensive." Small-batch production can push the price higher than virgin polyester, but large runs now approach parity. Compared to virgin nylon, you might pay a 10–15% premium, but you get a material that doesn't require new fossil fuel extraction and doesn't shed microplastics at the same rate in early washes. That trade-off matters more to some buyers than a marginal difference in color fastness.
Vetting Suppliers and Setting Your Own Specs
When you start working with a new factory, the vetting process goes far beyond checking a business license. Spend time asking for samples from their most recent production run, not just the polished prototypes they want to show you. Request references from clients in your product category and call them. Visit the facility if possible, or hire a local inspection service to walk the floor. Look for signs of consistent quality control: calibration stickers on equipment, organized raw material storage, and workers following written instructions. A supplier that hesitates to share audit results or deflects your questions about defect rates is often hiding capacity or consistency problems that will surface later.
Once you have narrowed the field, stop relying on vague phrases like high quality or standard thickness. Write down your own specifications with numbers, tolerances, and test methods. For example, state the exact material grade, surface finish, dimensions with acceptable plus/minus ranges, and packaging requirements. If a supplier says they can meet your spec, ask how they will verify it. Request a pre-production sample and a first-article inspection report. Keep your specs realistic; overly tight tolerances that do not affect performance only raise cost and rejection rates. Revisit the spec after the first few orders and adjust based on what you actually measure, not what the salesperson promised.
FAQ
It's a continuous filament yarn made from recycled PET (mostly post-consumer bottles) that has been engineered for high tensile strength and low elongation. Unlike standard textile polyester, which prioritizes softness and dyeability, this grade is drawn and heat-set to achieve tenacity levels around 7-9 grams per denier, making it suitable for load-bearing applications.
The process starts with sorting, washing, and flaking recycled PET bottles. The flakes are melted, filtered, and extruded through spinnerets. To reach high tenacity, the filaments undergo controlled drawing and heat stabilization. Quality checks on intrinsic viscosity ensure the recycled polymer retains enough molecular weight for industrial performance.
You'll find it in automotive seat belts and airbags, geotextiles for soil reinforcement, lifting slings, cargo nets, conveyor belts, ropes, and coated fabrics for tents and tarpaulins. Its combination of strength, abrasion resistance, and low stretch makes it a reliable alternative to nylon or virgin polyester yarn in demanding environments.
When properly processed, the difference is negligible. Modern recycling and solid-state polymerization can restore intrinsic viscosity to levels that match virgin polymer. The resulting yarn offers similar breaking strength, fatigue resistance, and UV stability. Some batches may show slightly higher variability, but reputable manufacturers control this tightly.
Each kilogram diverts roughly 1.4 kg of post-consumer PET waste from landfills or incineration. It also lowers energy consumption by 30-50% compared to virgin polyester production and reduces greenhouse gas emissions. Because it's a drop-in replacement, industries can switch without redesigning equipment or sacrificing performance.
The main challenge is maintaining consistent intrinsic viscosity and color. Contaminants from bottle labels or caps can cause spinning breaks or weak spots. However, advanced filtration and blending with higher-grade recycled flakes mitigate this. In critical applications like lifting slings, batch testing is advisable to confirm tensile specs.
Request technical data sheets showing tenacity (typically ≥7.0 g/den), elongation at break (usually 12-18%), shrinkage, and denier uniformity. Ask about the recycled content percentage and certification (e.g., GRS, Oeko-Tex). Also verify the UV resistance package if the yarn will be exposed outdoors.
Technically, polyester can be mechanically or chemically recycled multiple times, but each heat history degrades the polymer chain slightly. For industrial yarns that have been heavily coated or contaminated, mechanical recycling may be impractical. Chemical depolymerization offers a route back to monomers, though it's still scaling up. Designing for mono-material products improves end-of-life options.
Conclusion
Industrial high tenacity recycled polyester filament yarn turns a sustainability story into an engineering asset. Instead of settling for the lower strength often associated with recycled fibers, this material is engineered so that tenacity, controlled elongation, and abrasion resistance meet the demands of load-bearing and high-wear environments. The production path matters as much as the performance: post-consumer PET bottles are collected, cleaned, and extruded into filament with a consistent molecular orientation, which is what gives the yarn its high strength and dimensional stability. Because the recycled polymer is reprocessed under tight controls, the final filament avoids the weak points and inconsistencies that used to limit rPET to low-stress applications. The result is a yarn that can handle tension, friction, and repeated loading without sacrificing its recycled content or its mechanical integrity.
In industrial settings like cargo strapping, geotextiles, conveyor belts, safety nets, and heavy-duty sewing thread, this yarn competes directly with virgin polyester and even nylon. Against virgin polyester, it offers comparable tenacity at a lower environmental footprint, while against nylon it often shows better UV resistance, lower moisture regain, and greater dimensional stability in wet conditions. The key is not just the fiber itself but how suppliers are vetted: batch-to-batch consistency, documented tensile and elongation test data, and clear melt-flow specifications separate reliable sources from greenwashed alternatives. Buyers who set their own minimum tenacity, elongation at break, and abrasion benchmarks can use this recycled filament as a true drop-in replacement, reducing raw material impact without compromising safety margins or service life.
Contact Us
Contact Person: CONNIE
Email: [email protected]
Tel/WhatsApp: 86-0512-53671634
Website: https://www.lida-yarn.com/