OEM Stainless Steel Protective Film Factory Guide for Long-Lasting Protection
2026-08-28
Stainless steel looks indestructible—until a cheap protective film fails prematurely. If you’re sourcing OEM films, the factory you choose determines whether your surfaces stay flawless for years or become a costly liability. This guide draws on Shire’s production expertise to show you exactly what separates lasting protection from short-term cover.
How to Spot a Protective Film That Actually Protects
Most protective films look identical on a roll, so your first move is to check the spec sheet—thickness is the most honest number. A real guard layer should be at least 6 mils thick, but 8 mils or more is what you want for high-impact areas like hood edges and mirror caps. Anything thinner might feel smooth in your hand, yet it will tear or lift after a season of stone chips and automatic car washes.
Next, stretch a small sample between your fingers. A decent film won't whiten or snap under tension; it should recover its shape slowly. If the shop has a cured test patch, try scratching it with a coin. Films with elastomeric polymer backings often show shallow marks that fade with heat—either from the sun or a heat gun. If the scratch stays razor sharp, move on to another brand.
Finally, inspect the adhesive side. Run a fingernail across the edge: a quality adhesive will resist peeling at the corner but won't leave a gooey track when repositioned. Also read the warranty wording carefully. If it only covers "film failure" but excludes labor or yellowing, the manufacturer isn't fully confident. Trust films that have a documented five-year track record in your climate, not just polished demo clips.
The Unseen Steps in a Quality OEM Film Line
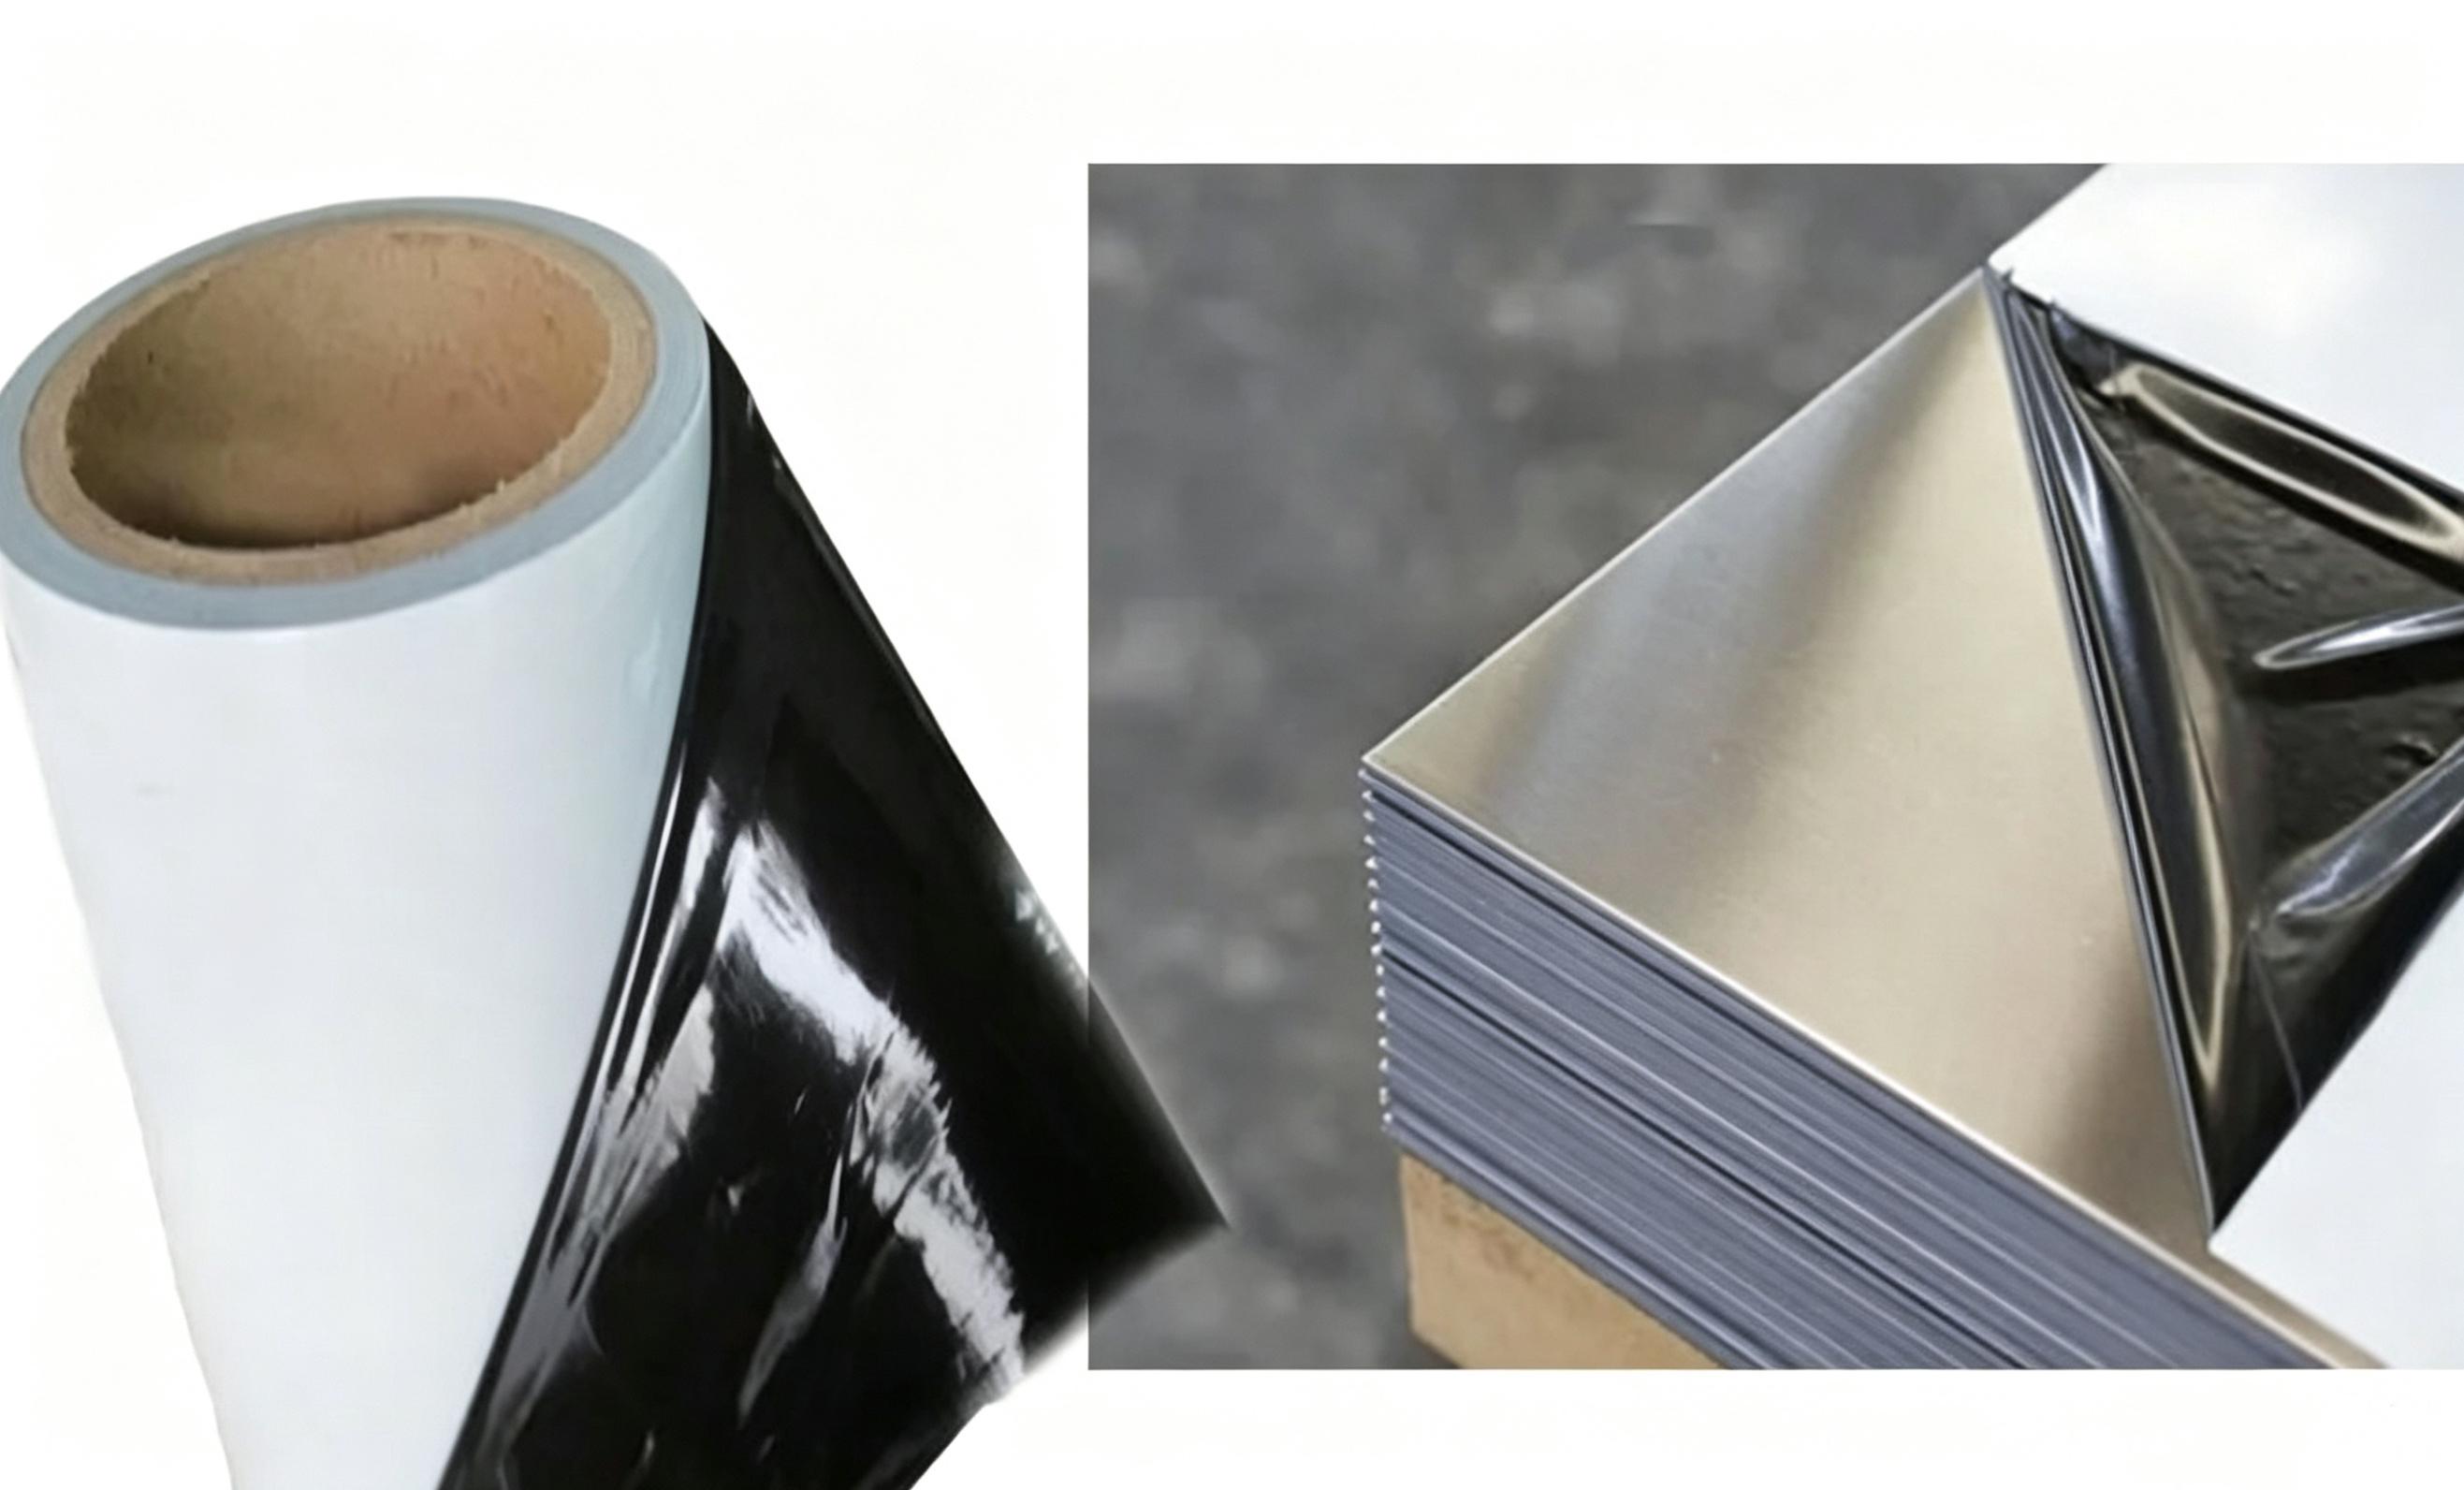
Walk into any film production facility and you'll notice something strange: the most critical work happens before a single frame gets shot. A quality OEM film line isn't just about the machines that coat and slit the material—it's about the quiet decisions made upstream. The raw substrate arrives with its own personality: how it breathes, how it holds tension, how it reacts to humidity. Miss those cues and every downstream process becomes a fight against the material rather than a collaboration with it.
Then there's the tension zone, that invisible band where the web stretches and relaxes between rollers. Operators who've run these lines for decades can feel a good setup just by touching the moving film with the back of a finger. It's not something you'll find in a manual. It's the accumulated instinct of watching thousands of meters behave—or misbehave—under slightly different air pressures, roller alignments, and drying temperatures. That's where a quality line hides its real value: in the hands that adjust a nip roll by half a millimeter because they know tomorrow's humidity will change everything.
Finally, the unseen step nobody talks about: failure analysis baked into daily routine. Not the dramatic kind, but the slow, patient study of edge beads, coating streaks, and static marks that appear only under certain light angles. A quality OEM line doesn't just produce film—it produces a living record of what the process tried to tell you. The best facilities treat every roll as a conversation, where the material speaks in faint visual dialects that only experienced eyes can translate into better tension profiles, cleaner adhesion, and fewer midnight call-outs.
Adhesive Chemistry: What Your Spec Sheet Won't Show
Most datasheets list lap shear strength and viscosity as if those numbers exist in a vacuum. They don't. The real chemistry happens at the interface, where a few monolayers of absorbed moisture or a trace of mold release can shift adhesion from structural to cosmetic. Even within the same adhesive family, the ratio of resin to hardener, the distribution of chain lengths, and the presence of unreacted low-molecular-weight species determine whether a bond creeps under load or stays put for a decade.
What's rarely printed is how the cured network responds to thermal cycling. A spec sheet may show Tg and elongation at break, but it won't tell you that a 10°C swing around the glass transition can generate enough internal stress to initiate microcracks at the bondline edges. Those microcracks then become pathways for moisture ingress, which plasticizes the polymer and lowers the effective crosslink density. The result is a joint that looks fine on day one but fails quietly after two years of seasonal temperature swings.
Batch-to-batch variation is another hidden variable. Raw resin suppliers change catalysts or adjust distillation cuts without flagging it downstream. Your incoming QC might catch viscosity drift, but not subtle shifts in amine value or epoxy equivalent weight that alter cure kinetics. In production, that translates to longer open times or incomplete cure at the same oven profile, leaving bonds that pass initial pull tests yet have compromised hydrolytic stability.
Why Some Stainless Steel Films Outlast Their Warranty
The durability of stainless steel films often comes down to how they handle microscopic stress. Unlike standard coatings that degrade from the surface inward, high-grade films form a self-healing oxide layer when exposed to air. This passive layer constantly rebuilds itself at scratches and edges, which means minor abrasions don't become starting points for corrosion. As a result, the film keeps its structural integrity long after the warranty period has technically ended.
Another factor is the raw material selection. Premium stainless steel films use a tighter grain structure with fewer inclusions and impurities. During manufacturing, controlled cold-rolling and annealing processes align the metal's crystalline lattice to resist peeling and cracking. This isn't just about thickness; it's about how evenly the film distributes tension. Films with uneven internal stress tend to fail early, while those with balanced stress can flex for decades without losing adhesion.
Finally, real-world performance hinges on the installation environment. When applied to a clean, properly prepared surface away from constant chemical exposure, the film's polymer backing and stainless layer work together to shed moisture and UV damage. Many installers underestimate how much surface prep affects longevity. A film that outlasts its warranty usually wasn't just lucky—it was matched to the right substrate and given a fighting chance from day one.
Factory Floor Decisions That Affect Long-Term Performance
Maintenance schedules often get squeezed when production targets loom, but the real cost shows up years later in unplanned downtime and worn-out equipment. Floor managers who treat preventive maintenance as a non-negotiable routine—rather than a luxury—tend to see steadier throughput and fewer emergency repairs that disrupt delivery promises. The same holds for operator training: a quick fix on a machine setting may save an hour today, but repeated shortcuts erode both part quality and the machine’s lifespan, quietly dragging down overall equipment effectiveness.
Another set of choices that compounds over time involves how work-in-process inventory is handled and how changeovers are managed. Allowing large batches to sit between operations may keep individual stations busy, but it hides bottlenecks, lengthens lead times, and ties up cash. Shops that invest in quicker setups and visual signals for replenishment usually find they can respond faster to customer changes without sacrificing long-term cost structure. None of these decisions feel dramatic on a single shift, but together they determine whether a factory builds capability or just burns through its assets.
Building an OEM Partnership That Survives the First Scratch
The first batch of enclosures landed on a Tuesday, and within an hour a line inspector had already circled a hairline mark near the USB cutout with a grease pencil. That single scratch, barely visible under shop lighting, quickly became a test of whether the partnership was built for shipping labels or for the messy reality of production. Most OEM relationships don't fail over big contract disputes. They erode in moments like this, when one side reaches for the spec sheet and the other reaches for the phone to argue about who pays for rework.
A partnership that survives the first scratch doesn't pretend scratches never happen. It builds a shared language for handling them before they appear. One electronics brand we worked with kept a physical "first article wall" in their vendor's factory, showing approved and rejected units side by side. When a new batch showed a subtle anodizing streak, the supplier's process engineer flew in the next day with cross-section photos instead of excuses. That turned a potential blame loop into a joint adjustment of rack spacing, and the next run was cleaner than either side had documented before.
What gets remembered isn't the scratch itself, but the speed and honesty of the response. Strong OEM ties treat each surface defect as an early signal, not a reason to trigger penalties. They set up weekly transparency calls that include line-level quality data, and they agree in advance who absorbs the cost of a first failed article while root cause is still unknown. Over time, that willingness to sit with an imperfect part and fix the process together leaves a deeper mark than any flawless first shipment ever could.
FAQ
Focus on how they control coating thickness and adhesive mixing, not just the extrusion line. Ask to see records for batch-to-batch viscosity checks and whether they test on actual stainless steel coupons rather than standard glass panels. A factory that can show real peel-adhesion data across different finishes like 2B, hairline, and mirror is far more credible than one that only talks about years of experience.
Ghosting usually comes from plasticizer migration or adhesive residues that oxidize at different rates than the metal surface. Cheap films with low-grade acrylic adhesives tend to break down under heat and UV, leaving a cloudy outline even after the film is peeled. A better factory will use cross-linked adhesives and low-migration backing films to avoid that permanent haze on stainless steel.
It is not just a matter of high tack versus low tack. Mirror finishes need a gentle but consistent wet-out so no air pockets form, while hairline and brushed surfaces require slightly higher initial tack to grip the texture without lifting at the grooves. The right OEM partner will ask for your exact finish spec and then adjust the adhesive coat weight and release liner stiffness accordingly.
Polyethylene is cheaper and fine for indoor storage or short transit, but it can become brittle and tear easily when stretched over curved stainless parts. Polyurethane costs more yet handles abrasion, forming, and UV exposure much better, which matters for architectural panels or appliances that sit outdoors for months. A factory that explains this trade-off instead of pushing one option is usually worth working with.
Yes, if they understand elongation and recovery rates. You need a film with enough stretch to follow the bend radius without snapping back and pulling away from the stainless surface. Ask for samples that have been bent on the same gauge and radius as your product, then check for edge lift after 24 hours at room temperature. That simple test tells you more than a spec sheet full of tensile numbers.
Request accelerated aging data that shows peel force after heat, humidity, and UV cycles, not just at day one. Also ask whether the film leaves any residue on passivated or electro-polished stainless, since those surfaces are more sensitive to adhesive transfer. A dependable factory will offer a removal guarantee tied to a specific time window and environmental exposure, rather than just saying it removes cleanly.
Ask for the test method behind the number. A realistic life claim is based on outdoor weathering tests in a region similar to your end-use climate, with photographic evidence of the film still intact and removable at the stated interval. If the factory cannot show test panels or only cites accelerated lab hours without correlation to real outdoor months, treat the figure as a rough estimate rather than a promise.
Conclusion
Most stainless steel protective film failures don’t happen on the job site—they start with a spec sheet that hides more than it reveals. A film that truly protects shows its pedigree in the details: uniform cast or calendered base layers, edge flatness that prevents lifting, and adhesive chemistry tuned to the exact surface roughness of your stainless finish. On a quality OEM line, you won’t see shortcuts. Clean-room slitting, tension control across wide webs, and corona treatment before coating are the unseen steps that determine whether the film peels cleanly after months of UV and temperature cycling. The adhesive itself is the quiet differentiator. Low-grade tackifiers can migrate or haze the metal, while a properly crosslinked acrylic or rubber system holds without building aggressive peel strength over time.
Long-term performance is decided before the roll ever ships. Factory decisions—like using virgin resins instead of recycled blends, matching liner release values to the adhesive’s cure curve, and rejecting any coating thickness variation beyond a few microns—separate a film that outlasts its warranty from one that fails at the first temperature swing. The strongest OEM partnerships don’t begin with a purchase order; they begin with shared test data, surface energy measurements, and a factory willing to walk you through their failure analysis instead of hiding behind a datasheet. When your supplier treats each change in stainless finish or storage climate as a reason to revalidate, not just reorder, you get a film that survives the first scratch—and the hundredth.
Contact Us
Contact Person: Jack Xu
Email: [email protected]
Tel/WhatsApp: 8615257328825
Website: https://www.temporaryprotectivefilm.com/