PVC Pipe Production Line Factory Essentials for Consistent Quality and High Output
2026-10-13
Ask any plant manager what keeps them up at night and it usually isn't the extruder—it's the slow drift in wall thickness, the jammed haul-off, the batch that runs fine until 2 a.m. High-output PVC pipe production is rarely about buying a bigger machine. It's about getting the factory-level essentials right so quality stays repeatable across every shift. That's where field experience from COMRISE lines comes in, and what this guide unpacks.
Nailing the Dry Blend Before It Melts
Most home cooks rush this stage, treating the dry blend as a mere formality before the liquid hits the pan. That's exactly where the flavor falls apart. You want every grain of spice, every fleck of herb, every crystal of salt to cling to the meat or vegetables before any moisture shows up. If you dump it all in at once and stir half-heartedly, you'll end up with pockets of raw cumin in one bite and bland nothing in the next. Work in small pinches, using your fingers to rain the blend evenly across the surface. Then—this is the part nobody tells you—let it sit for a full minute. The dry heat draws out the oils locked inside the spices, and that brief rest is what transforms a dusty coating into a crust that actually sticks.
Once that initial coat has settled, resist the urge to toss everything straight into the pot. Instead, take the back of a spoon or your palm and press the dry mix firmly into the ingredient. Not a violent smash, just a steady, deliberate push. That contact creates micro-abrasions on the surface, giving the blend something to bite into. If you're working with something porous like tofu or chicken thigh, the spices will start to seep in almost immediately. For denser cuts like beef or root vegetables, a second light dusting after the first press can make all the difference. The goal isn't more powder; it's better distribution. You're building a layer that will survive the first splash of liquid rather than floating away the moment broth hits the pan.
The real test comes the second the wet ingredients enter. If your dry blend was nailed, you'll hear it sizzle against the hot surface instead of dissolving into a sad paste. That sizzle is the sound of the outer layer setting into a fragrant shell. Don't stir immediately—give it ten to fifteen seconds of contact heat. Let the sugars in the spices caramelize just a touch, the pepper bloom, the garlic turn nutty. Then, when you finally do stir, the blend won't melt into the sauce; it'll break apart in rough, flavorful chunks that keep revealing themselves as you eat. That's the difference between a dish that tastes seasoned and one that tastes alive.
Barrel Zones That Stay in Sync
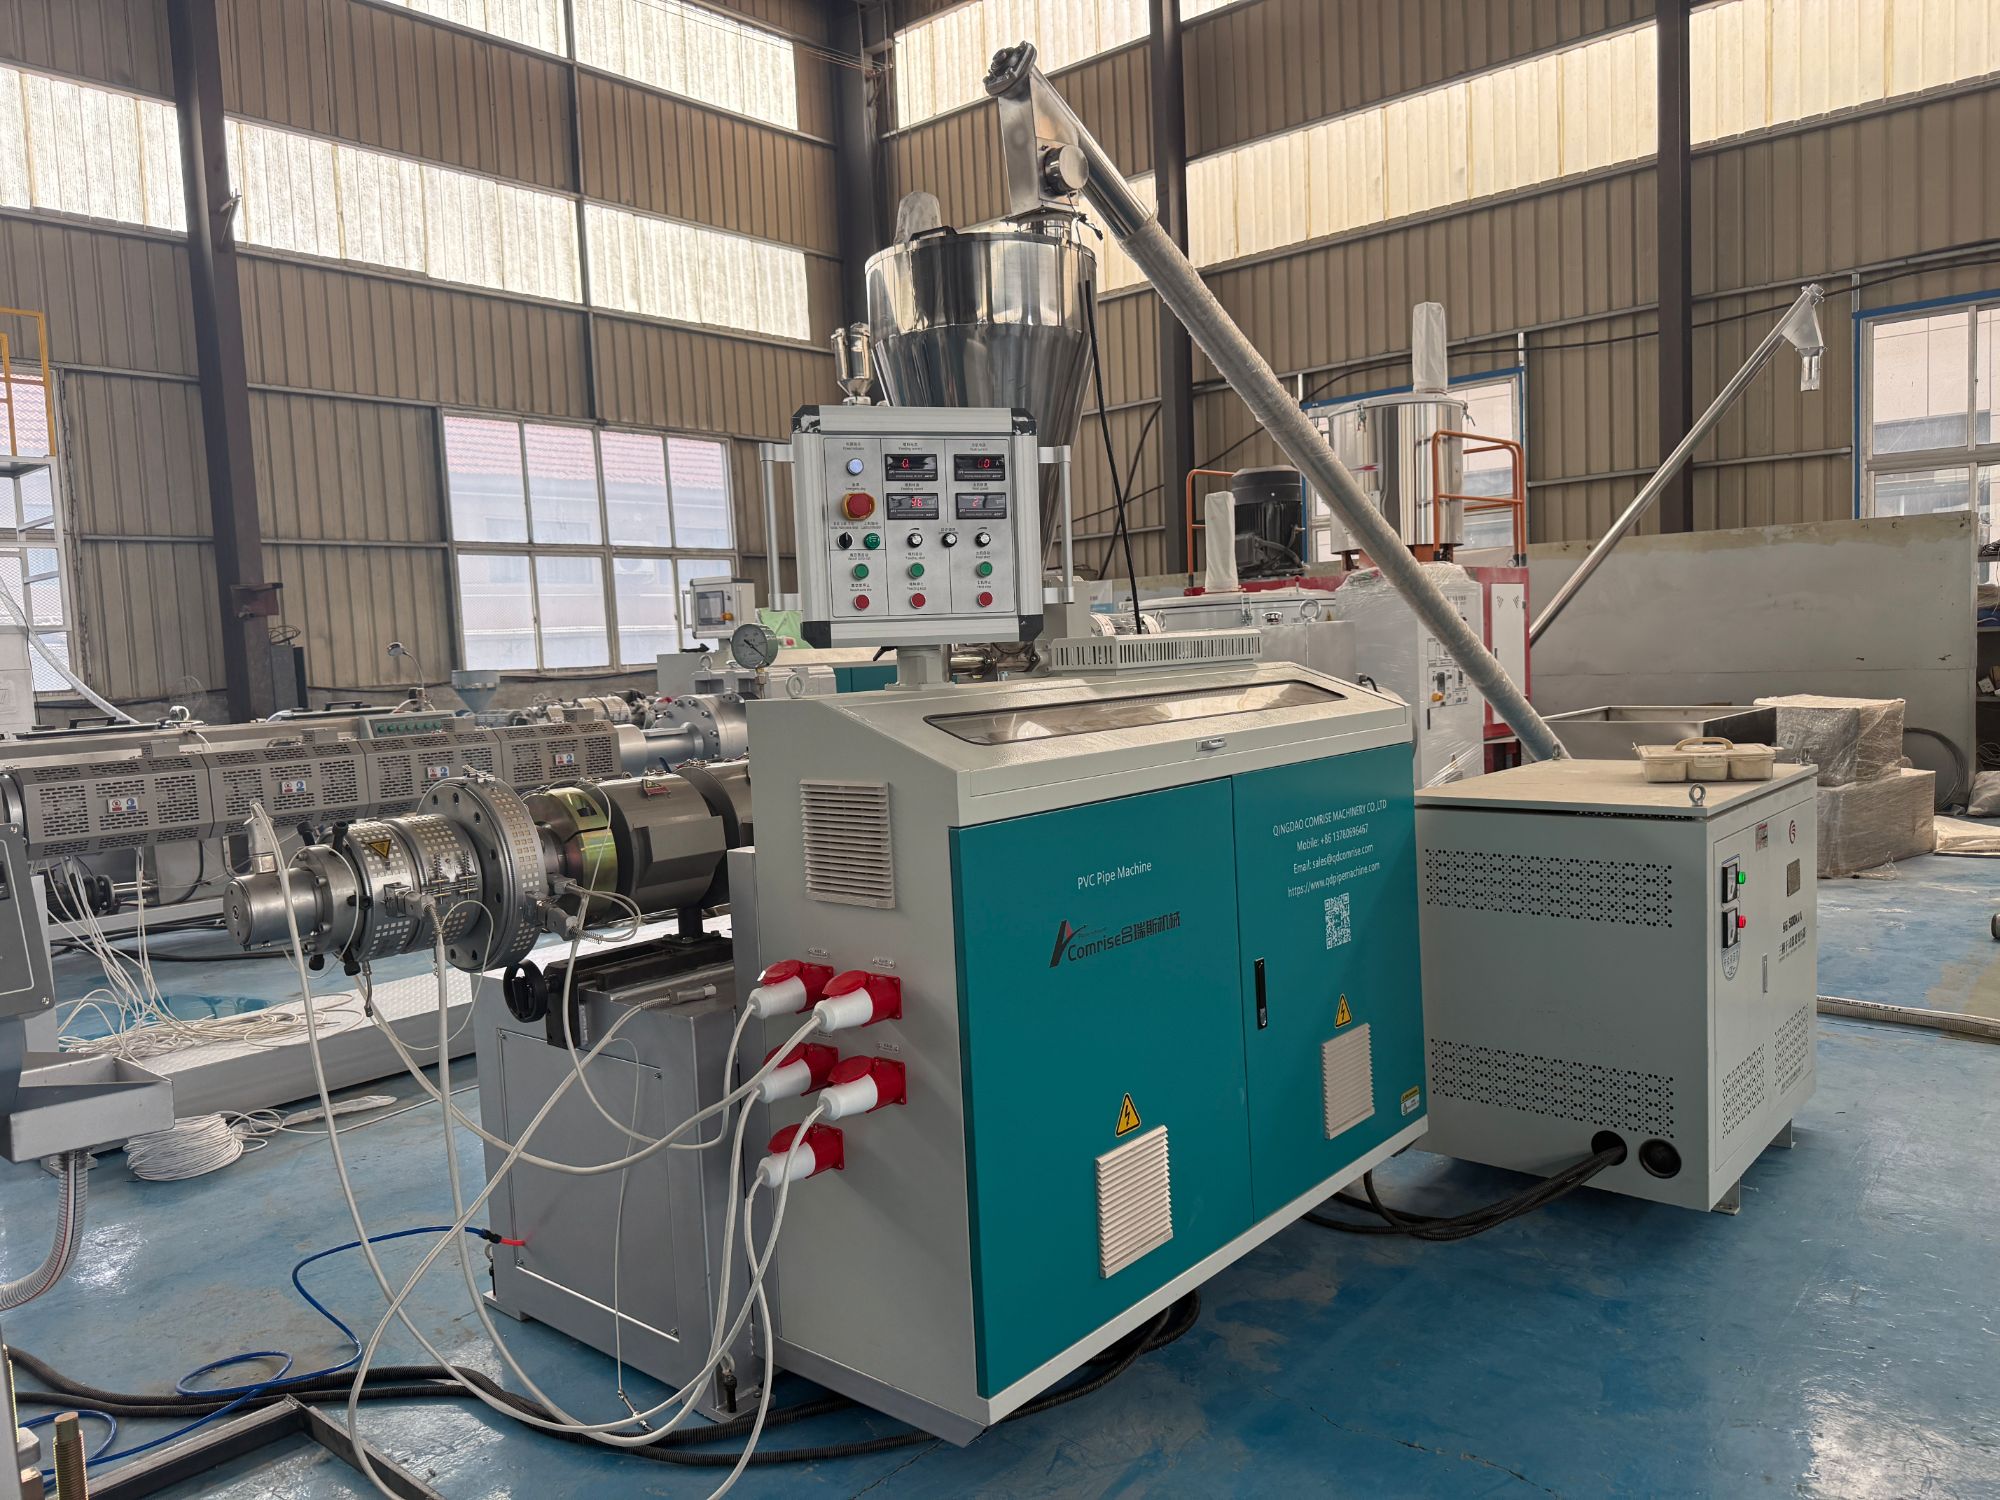
In a well-tuned barrel, the zones work less like isolated chambers and more like a group of musicians who have played together for years. The throat, the shoulder, the belly, and the muzzle each have their own job, but they trade energy back and forth without a single hiccup. When one zone tightens, the others adjust almost before the change happens. That kind of fluid handoff is what separates a barrel that feels alive from one that simply holds liquid.
Keeping those zones in sync often comes down to how the barrel is handled during its first few weeks of use. A slow, even break-in lets the wood settle into a shared rhythm. Rushed fills, sudden temperature swings, or uneven cleaning can throw one zone slightly ahead of the rest. Once that drift starts, you feel it as a faint vibration or a note that wavers on the draw. Many experienced users pay more attention to the barrel's breathing than to any single measurement.
There is also a quiet advantage to barrels that stay in sync: they age more gracefully. Rather than developing a strong zone next to a weak one, the whole surface wears at a matched pace. Subtle ridges and micro-changes appear together, which gives the barrel a smooth, predictable character over time. That is not something you can force with a machine, and it rarely shows up in a spec sheet. It comes from patient use and a willingness to listen to what the barrel is already doing.
The Die Face You Can't Afford to Ignore
Most press operators can recite cycle times and tonnage figures without a second thought, but ask about the condition of the die face and you’re likely to get a shrug. That surface—where material flows, stretches, or solidifies under load—has more say in part quality than any single machine setting. If it’s worn, pitted, or unevenly stressed, every “minor” adjustment you make elsewhere is just compensating for a problem that keeps growing.
Ignoring the die face rarely causes immediate failure. Instead, you’ll see a slow creep of defects: micro-cracks that open into galling, heat checking that roughens the finish, or localized adhesion that tears material. By the time these signs become obvious, the die already needs more than polishing. Replacement inserts, re-machining, and unplanned downtime eat into margins that could have been protected with a ten-minute inspection after each run.
The fix isn’t complicated, but it does require consistency. Check for visual wear under raking light, measure key radii, and record any buildup or discoloration. Use coatings or surface treatments that match your material type, and don’t let small scratches become excuses for “production over maintenance.” A die face that gets regular attention will outlast one that only gets noticed when scrap rates spike.
Vacuum Calibration Without the Guesswork
Instead of adjusting a vacuum gauge until it matches another one and hoping for the best, calibration should rely on physical references. A known volume with a precision capacitance diaphragm gauge can serve as a transfer standard. By controlling the gas inlet and measuring pressure rise over time, you can determine the actual pressure and compare it to the sensor output. This removes most of the trial and error.
Temperature and gas species affect readings. So a robust calibration routine includes recording ambient temperature and making corrections for thermal transpiration if the sensor operates at a different temperature than the reference. Ignoring these factors leads to offsets that shift with operating conditions, not a fixed zero or span error.
Some setups use a spinning rotor gauge or a quartz friction gauge as a secondary standard because they stay stable over long periods. The goal is to map the sensor's response across its range, not just at one point. That way, you get a curve you can trust, not just a single number that may only be valid under one condition.
Pull and Cut Timing That Prevents Jams
Most jams blamed on dull blades are actually timing problems. When the cutter fires before the pull stroke has fully stopped, the material is still under tension and can shift sideways, crumple, or fold over the blade. Let the pull finish, wait a beat, and then cut. That short pause lets the media relax flat, so the knife slices through instead of shoving against a moving edge.
If your machine allows timing adjustment, don't set it by guesswork. Start with an obvious delay, then shorten it in small steps while watching the exit path. The moment you see a slight hesitation or hear a sharper snap, back off to the previous setting. This gives you a margin that absorbs small variations in media thickness or roll tension, which are exactly what turn a good setting into a jam on a different day.
Inline Checks That Stop Defects Early
Most developers don’t enjoy discovering a bug three days after they wrote the code. Inline checks flip that timeline by catching type mismatches, null dereferences, and questionable API usage directly in the editor as you type. That immediate signal means you fix issues while the context is still warm, usually in seconds instead of after a lengthy test cycle or code review.
The real power comes from tuning the checks to your team’s actual failure patterns. Instead of drowning people in style warnings, focus on the handful of rules that have historically caused production incidents—things like unsafe deserialization, missing error handling on external calls, or resource leaks. A good inline checker can spot these before a commit ever leaves your machine, and modern language servers make it fast enough to feel invisible.
Teams that adopt this approach often notice that code reviews shift from hunting for mechanical mistakes to discussing architecture and trade-offs. That doesn’t happen by accident; it requires periodic pruning of rules that generate too much noise and pairing the checks with a quick way to suppress false positives. When the signal-to-noise ratio is right, inline checks stop feeling like a gate and start acting like a second pair of eyes.
FAQ
Incoming resin and additives should be tested for bulk density, moisture content, and particle size before they reach the hopper. Even small shifts in stabilizer or lubricant levels can alter fusion and surface finish, so many plants pre-blend materials and verify each batch against a reference formulation.
PVC degrades quickly if overheated but fails to fuse properly if too cold. The barrel usually runs hotter near the feed throat to start gelation, then tapers to a lower front zone to prevent scorching. Operators should record zone-by-zone readings and adjust only one zone at a time to avoid chasing temperature swings.
Pull the screw every 3,000 to 5,000 operating hours, or sooner if output drops or melt pressure rises. Look for wear on the flight lands and root diameter, and check the barrel for scoring. Preventative replacement is cheaper than a mid-run failure that sends off-spec pipe to scrap.
The vacuum tank holds the hot pipe against sizing sleeves while water cools it. Keep the vacuum steady—usually between -0.2 and -0.6 bar depending on pipe size—and maintain water temperature within a narrow band. Fluctuations here cause ovality, poor wall distribution, and lengthwise ridges.
Haul-off speed must match extruder output; if it pulls too fast, wall thickness drops, while too slow creates thick spots and internal stress. Set the cutter to activate on a length encoder, not a timer, and keep the stacking table speed slightly below line speed so pipes don't jam or scuff.
Watch the melt pressure and motor load. A sudden drop in pressure with the same screw speed often means over-lubrication, while rising pressure and a rough surface point to under-lubrication or insufficient stabilizer. Frequent lab checks of heat stability and color also catch drift before it becomes visible scrap.
Use ultrasonic gauges at several points around the circumference, not just one fixed location, and compare readings to a master ring. Calibrate the gauge against a known step wedge daily, and reset it after any change in resin lot or colorant because acoustic velocity shifts slightly with density.
A skilled operator reads trends—like a slow rise in head pressure or a faint surging sound—before they turn into rejects. Cross-training on start-up, die changes, and troubleshooting reduces downtime, and documented settings per product avoid the tribal knowledge trap when shifts change.
Conclusion
Achieving consistent quality and high output on a PVC pipe production line starts well before the extruder reaches full temperature. The dry blend must be perfectly homogenized—resin, stabilizer, and additives dispersed evenly—otherwise you'll chase melt variations all shift. Once flowing, barrel zones need to work as one thermal unit; a lagging middle zone or an overdriven feed throat creates surging that shows up as wall-thickness drift. The die face is where many lines quietly lose money: uneven land lengths or worn chrome let one side of the pipe run faster, forcing operators to over-correct downstream. Skilled teams learn to read the melt pressure curve and make small die adjustments before the problem reaches calibration.
Vacuum calibration is not a set-and-forget step. Sizing sleeves and water flow must match the exact shrinkage rate of your formulation, otherwise you get ovality or drag marks that only appear after cutting. Puller speed and saw timing need to be tuned as a pair—too much tension stretches the pipe while it's still soft, and a mistimed cut can crush the leading edge and jam the haul-off. Finally, inline checks like ultrasonic wall measurement and diameter gauges should trigger alerts the moment a trend drifts, not after a full bundle is packed. Factories that treat these six areas as one connected system—not isolated stations—consistently hit higher line speeds with fewer rejects.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com