Top 10 ABB Electromotor Picks for Reliable Industrial Performance
2026-09-25
When industrial operations demand motors that won’t let you down, ABB remains a go-to name—but with so many options, narrowing down the best Electromotor models can feel overwhelming. In this guide, we’ve distilled the top 10 ABB picks for dependable, high-performance industrial use, each evaluated for torque, efficiency, and real-world durability. Whether you’re retrofitting a production line or planning a new installation, these selections cut through the noise. And for teams seeking hands-on sourcing support or alternative OEM-compatible units, Soochee offers practical guidance worth exploring alongside ABB’s renowned lineup.
Cast Iron Frames That Survive Vibration-Heavy Conveyor Lines
Most conveyor frame materials break down quietly at first—hairline cracks near bolt holes, loosened fasteners, a subtle wobble that grows into misalignment. Cast iron behaves differently. Its dense grain structure and inherent damping capacity absorb the constant, low-frequency shaking that comes from vibrating screens, crushers, or sorting decks. Instead of transmitting every jolt down the line, the frame dissipates that energy as heat, keeping joints tight and alignment intact far longer than welded steel or extruded aluminum in the same environment.
Field crews often notice the difference during routine inspections. A cast iron frame may show surface oxidation or caked-on dust, but its mounting points stay rigid. Tension bolts don't back out; bearing seats don't ovalize. That reliability comes from the material's high modulus and natural resistance to fatigue loading—properties that don't require extra gussets, dampers, or frequent retorquing. When a line runs two shifts a day with heavy product surging across it, the frame's ability to simply hold its shape becomes the difference between scheduled maintenance and emergency downtime.
Not every cast iron frame earns a place on a vibration-heavy line, though. The best designs use thick flanges, tapered ribs, and generous radii at stress points, avoiding sharp corners that invite crack initiation. Pair that geometry with a properly bedded foundation or isolation mounts, and you get a structure that shrugs off the pounding that would rattle a lighter frame apart in six months. For plants tired of chasing alignment issues, swapping to cast iron isn't an upgrade—it's the baseline for keeping the conveyor running straight while everything around it shakes.
IE4 vs. IE5: Which Tier Pays Back Faster in Continuous Duty
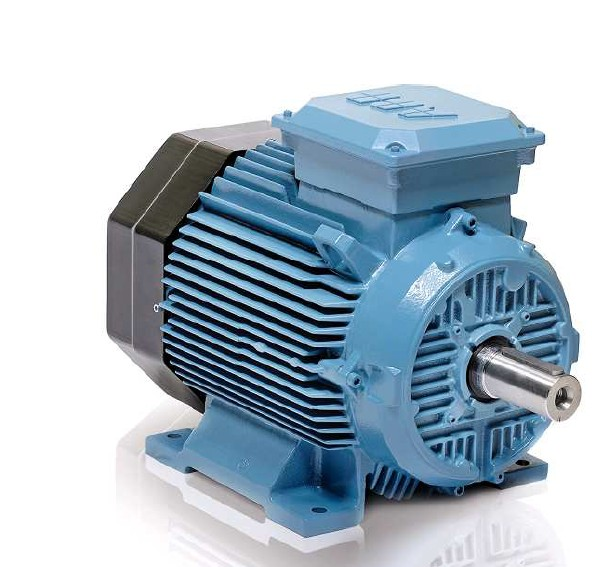
When a motor runs around the clock, the math behind efficiency tiers gets brutally simple. IE5 units carry a price premium that makes procurement teams wince, but they also shave losses to the bone. On a 75 kW machine logging 8,000 hours a year, the delta between IE4 and IE5 often amounts to a few thousand kilowatt-hours annually. At industrial power rates, that gap closes the upfront cost difference within two to three years on most frame sizes—sometimes faster if the local utility tacks on demand charges.
The catch is that continuous duty doesn't mean constant load. Many so-called "continuous" applications throttle back or idle for stretches, and partial-load efficiency curves narrow the gap between tiers. In those cases, IE5 might take an extra season or two to hit breakeven. But for pumps, fans, and compressors humming at 75% load or better without scheduled downtime, the premium motor typically starts printing savings well before the first bearing replacement. Factoring in rising electricity costs, the smarter bet is usually the higher tier—provided the process truly never sleeps.
Low-Speed, High-Torque Designs for Mixers and Crushers
Mixers and crushers often face materials that resist movement—thick pastes, heavy slurries, or coarse aggregates. A low-speed, high-torque design keeps the rotor or auger turning steadily even when load spikes, preventing stalls and reducing the need for oversized motors. This approach relies on deep gear reduction and robust shaft connections, which transfer power smoothly rather than relying on raw RPM.
In practice, the torque curve becomes more useful than peak horsepower. A crusher fed with uneven chunks of rock or demolition waste sees rapid changes in resistance; high torque at low revs lets the crushing surfaces bite through without slipping belts or tripping overloads. Mixers handling viscous compounds, such as heavy adhesives or mineral slurries, benefit similarly because the agitator can maintain a consistent shear rate without overheating the drive train.
Maintenance also shifts in favor of this design. Lower speeds mean less wear on bearings, seals, and cutting edges, while the high torque rating allows direct coupling to the load—eliminating fragile chain or belt drives. For operators, that translates into fewer unexpected shutdowns and a longer service life for the core rotating assembly.
Built-In Vibration Sensors That Flag Bearing Wear Early
Rather than relying on handheld probes or bolted-on accelerometers that often pick up noise from surrounding machinery, these sensors sit directly inside the bearing housing. That placement puts them close enough to catch the faint, high-frequency ringing that occurs when a raceway first starts to spall or a rolling element develops a micro-pit. The result is a warning that arrives weeks or even months before the damage becomes audible to the human ear or visible in a temperature trend.
The real value comes from continuous trending, not one-off measurements. Because the sensor is always listening, it builds a vibration signature for each bearing under normal load and speed. When the system detects a repeatable spike at a known fault frequency—say, the ball pass frequency of the outer race—it can flag that specific bearing before roughness grows into a full-blown failure. Some setups also track high-frequency demodulation or acceleration enveloping, which makes the early-stage signals stand out from the low-frequency rumble of gears and shafts.
For plants that already run lean on maintenance staff, this built-in approach removes the need for scheduled route-based vibration checks. The sensor and its local processor handle the listening and the math, pushing only actionable alerts to the control room or a maintenance app. That cuts down on false alarms while giving technicians a clear head start on ordering replacement bearings and planning a short, controlled shutdown instead of dealing with an unplanned line stop.
Motors Rated for Frequent Washdowns and Corrosive Air
In food processing plants, breweries, and chemical handling facilities, standard motors quickly degrade under high-pressure spray cleaning or exposure to airborne acids and salts. Motors built for these conditions feature fully sealed housings, stainless steel shafts, and epoxy-coated windings that shrug off moisture and chemical attack. Instead of relying on external paint alone, the frame itself often uses 300-series stainless or a specialized polymer blend to prevent rust from starting at scratches or joints.
Frequent washdowns demand more than just water resistance—every joint, fitting, and cable entry must handle thermal shock from hot sanitizing solutions followed by cold rinse cycles. These motors incorporate double-lipped shaft seals, O-ring gaskets on end bells, and pressure-equalizing breathers that keep vapor out while letting internal condensation escape. The result is a drive unit that keeps spinning through daily caustic foam baths and chlorine fog without bearing failure or winding shorts.
Beyond stainless exteriors, corrosive-air-rated motors often use ceramic hybrid bearings and sealed terminal boxes filled with potting compound to lock out hydrogen sulfide, ammonia, or salt spray. Drain holes are positioned away from the washdown stream, and nameplates use laser etching rather than adhesive labels that peel after repeated chemical contact. For operations where a failed motor means shutting down an entire processing line, this level of protection pays for itself within the first year of uninterrupted service.
Retrofit Kits That Bring Older Machines Up to Current Efficiency Rules
A well-designed retrofit kit often starts with a detailed audit of the machine's existing fuel, hydraulic, and cooling circuits. By swapping in electronic governors, high-pressure common rail injectors, or variable-displacement pumps, a 20-year-old excavator or wheel loader can meet current emission and efficiency rules without the capital cost of a new unit.
Many kits also include aftertreatment add-ons such as diesel particulate filters or selective catalytic reduction dosing, along with recalibrated engine control modules. The installation can be completed during a routine rebuild, and the gains typically show up as lower idle fuel consumption, reduced heat rejection, and fewer regeneration cycles, which keeps older fleets legally operable in regulated regions.
FAQ
The M3BP series often hits that sweet spot. It is built with cast iron housing and high-grade insulation, so it holds up well in demanding environments without an extreme price tag.
Go with aluminum if weight matters and the environment is clean. Cast iron makes more sense when there is moisture, dust, or mechanical stress, since it handles rough conditions better.
They reduce energy losses through better rotor and stator design. Over a typical service life, the savings on electricity often cover the price difference several times over.
Yes, most of them are designed with inverter-duty insulation and cooling that works well at lower speeds. Just check the specific model's speed range and forced cooling requirements.
Keep the cooling fins clean, check bearing lubrication on schedule, and monitor vibration and temperature trends. Catching small changes early prevents most unexpected failures.
Look at their stainless steel or fully enclosed fan-cooled options with IP66 rating. These are sealed against water jets and resist corrosion better than standard motors.
The M2BA generally offers higher efficiency and improved cooling. It is dimensionally compatible in most cases, but you should confirm shaft height and mounting dimensions before swapping.
Start with the load curve and required air flow. Then match the motor's continuous torque capability to the fan's demand at operating speed, leaving at least 10-15% headroom for voltage drops and wear.
Conclusion
When equipment runs on a vibrating conveyor line or inside a food plant with daily caustic washdowns, motor choice is less about nominal specs and more about survival. ABB's strongest performers in these conditions pair cast iron frames with reinforced bearing housings, so shaft alignment holds even when the mounting plate is shaking. For wet or corrosive air, fully enclosed designs with sealed lead exits and epoxy-coated windings keep moisture and chemicals out of the insulation. Integrated vibration sensors add a practical layer: instead of waiting for a bearing to scream, maintenance teams see trend data early and swap parts during planned downtime. That combination of mechanical stiffness and sensor feedback turns a routine motor into a condition-monitoring node on the plant floor.
Efficiency decisions are equally grounded. IE4 may cost less upfront, but in continuous duty the extra losses can erase the difference within two or three years depending on local energy prices and load profile. IE5 units often pay back faster in 24/7 processes, while low-speed, high-torque designs for mixers and crushers avoid gearbox losses altogether, running direct at 100–200 rpm. Older machines don't need to be left behind either: retrofit kits with new rotors and fans bring legacy frames up to current efficiency rules without changing mounting dimensions. The result is a short list that covers both new installations and upgrades, where each pick earns its place by cutting energy waste, extending bearing life, or simplifying washdown upkeep.
Contact Us
Contact Person: Jenny Jaa
Email: [email protected]
Tel/WhatsApp: 0086 152 9510 6006
Website: https://www.china-motor-supplier.com